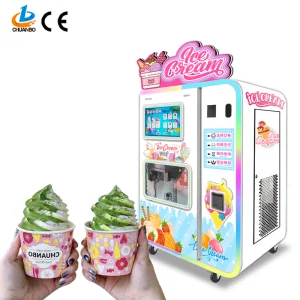
CN Soft Serve
The global restaurant equipment and commercial food machinery sector is undergoing a profound paradigm shift driven by labor optimization, strict hygiene mandates, and automated self-service technologies. Modern catering enterprises, global retail franchises, and entertainment complexes demand high-efficiency, IoT-enabled, and cloud-managed equipment that guarantees seamless round-the-clock operations with minimal human intervention. As a top-tier factory and supplier, meeting these multifaceted industrial requirements necessitates rigorous engineering standards, scalable production lines, and advanced quality verification frameworks.
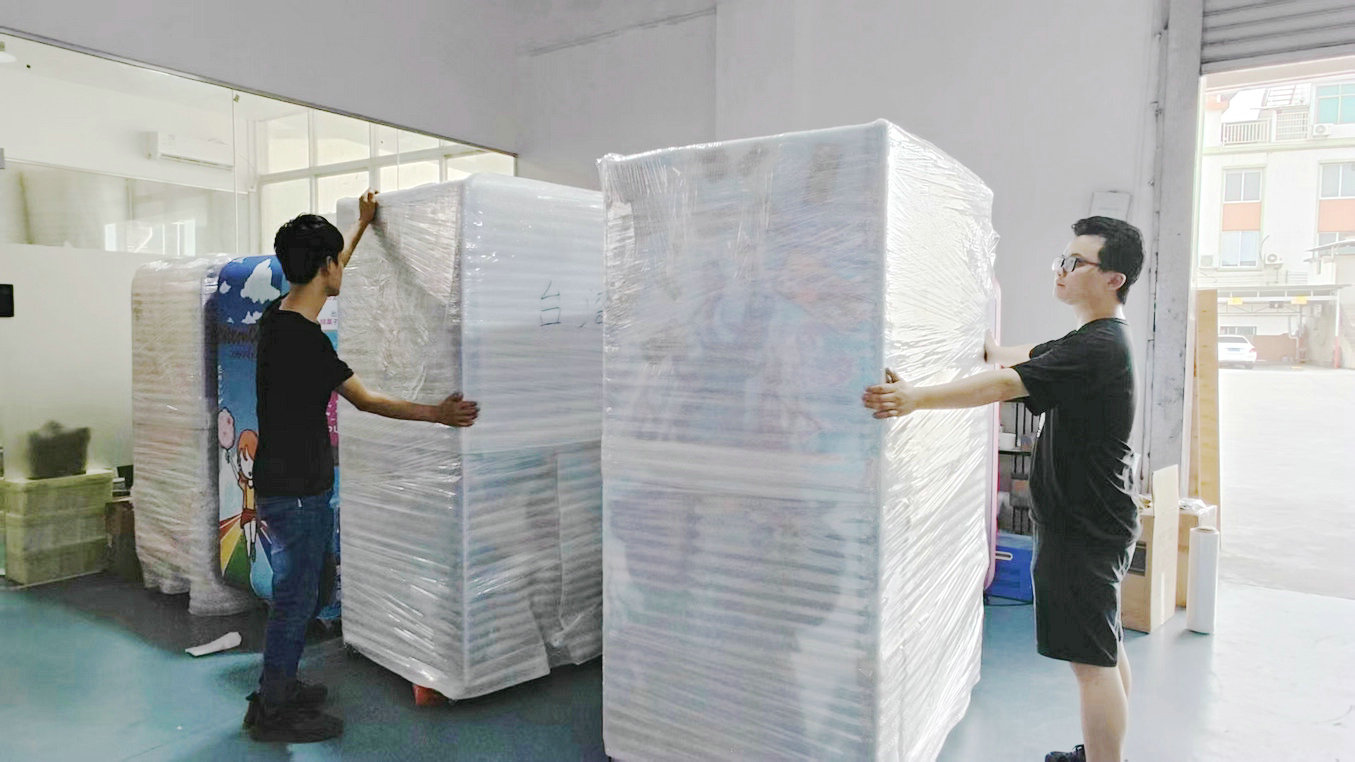
China's manufacturing clusters provide an unparalleled advantage in the restaurant equipment sector. By integrating robust metallurgy, precision compressor engineering, and advanced IoT software development, top-tier factories achieve optimal economies of scale without compromising on quality. Raw material traceability, automated sheet-metal fabrication, and stringent pre-shipment aging tests ensure that every unit leaving the assembly line meets international safety standards including CE, UL, RoHS, and CB. Global B2B buyers benefit from direct-factory pricing, agile custom development (OEM/ODM), and robust supply chain resilience.
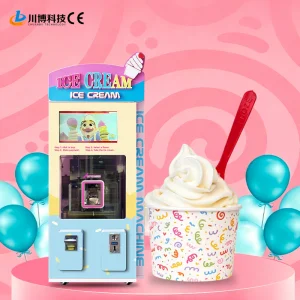
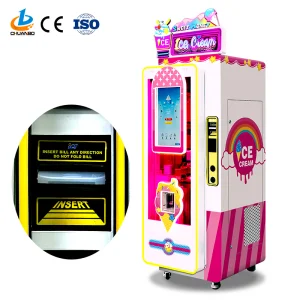
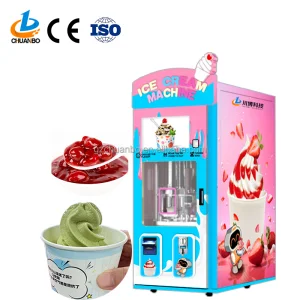
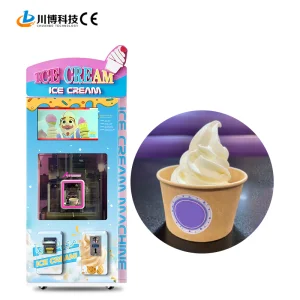
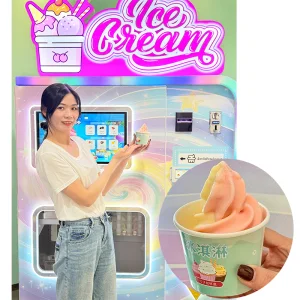
Commercial refrigeration and automated food dispensing systems are deployed across diverse high-traffic environments, ranging from North American shopping malls and South American amusement parks to Middle Eastern hospitality venues. Modern operators prioritize unattended 24/7 business models equipped with cashless payment gateways (Coin, Bill, Credit Card, Nayax, QR Code integration) and cloud-based telemetry software. This real-time inventory and performance monitoring reduces maintenance overhead and maximizes revenue generation per square meter.
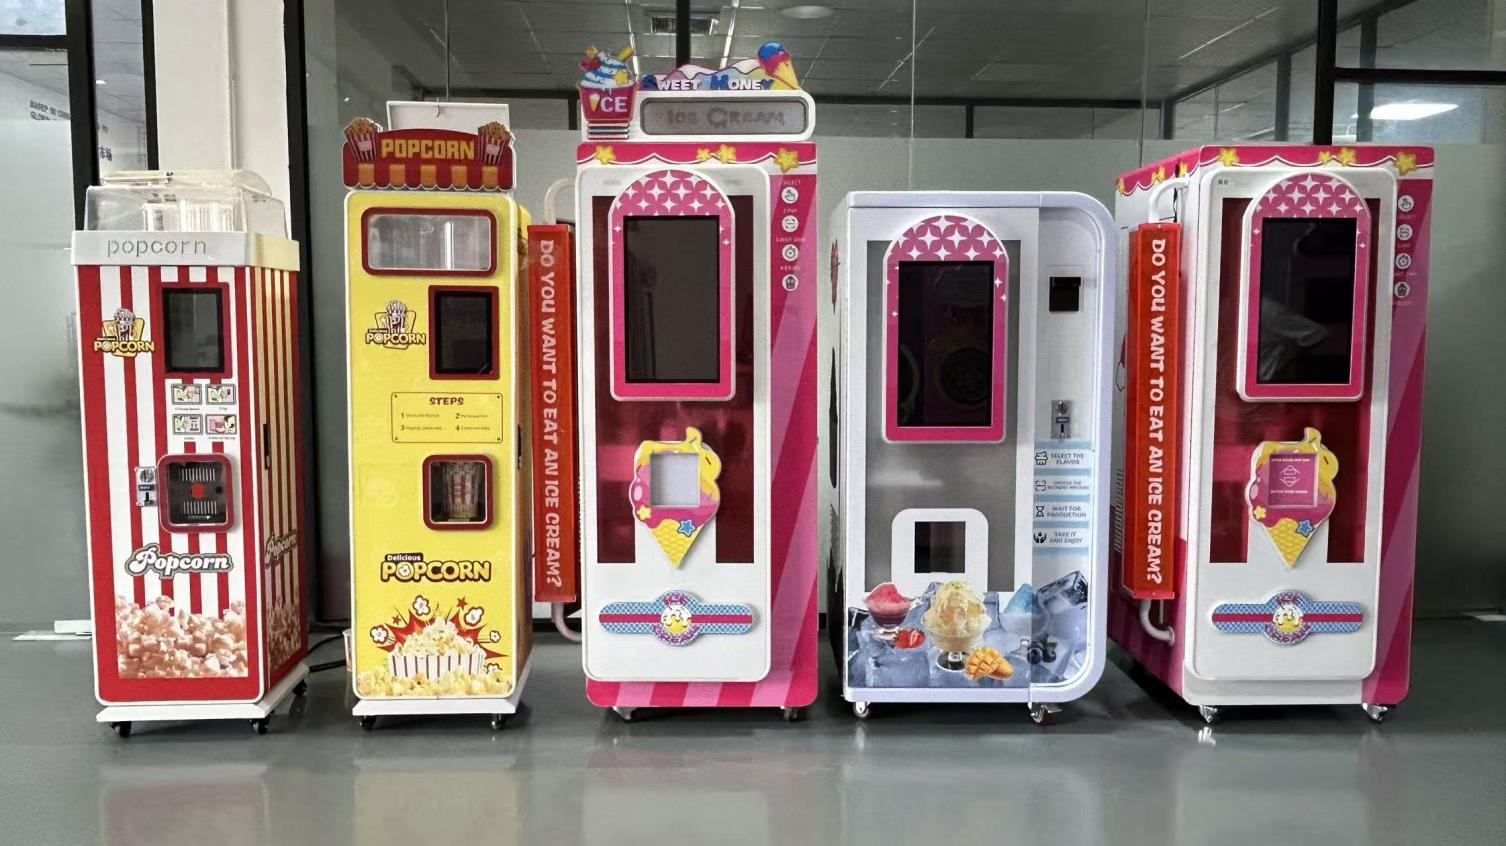
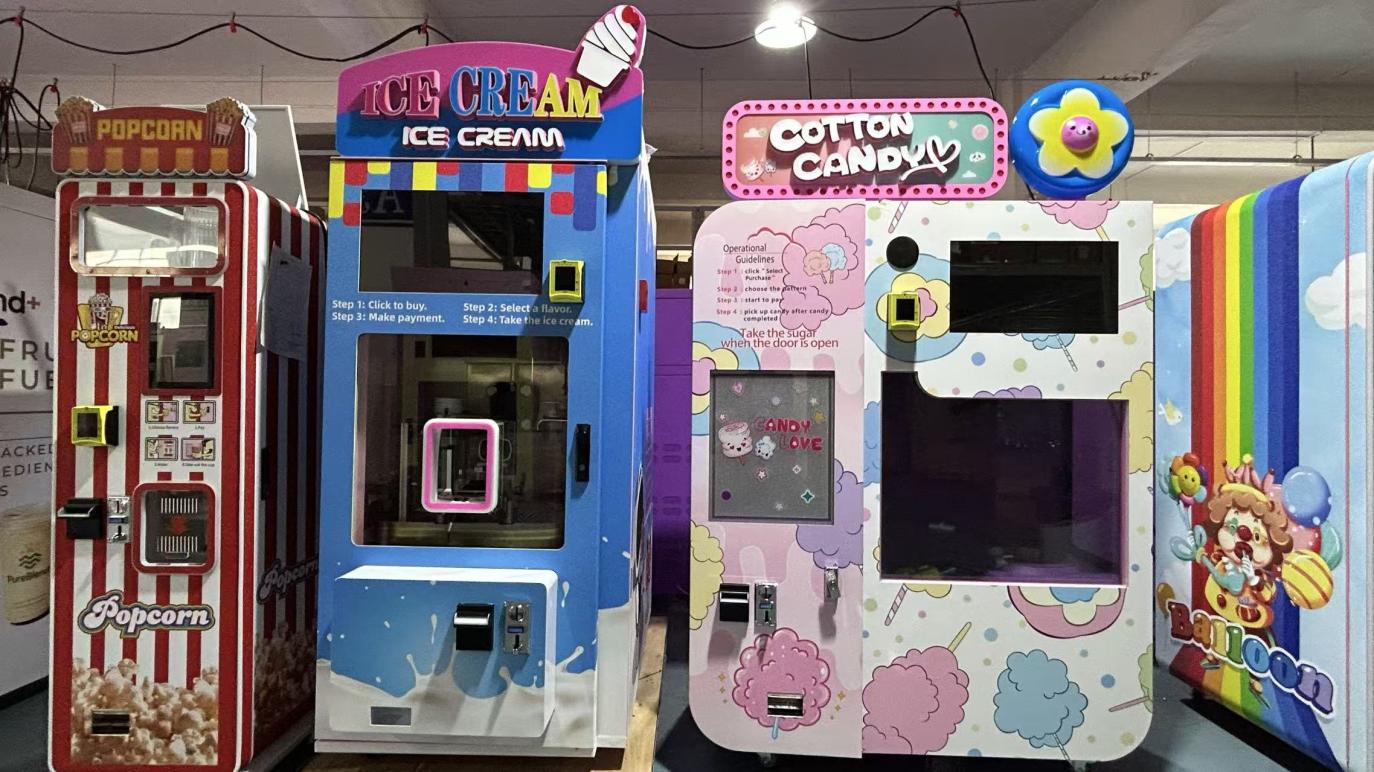
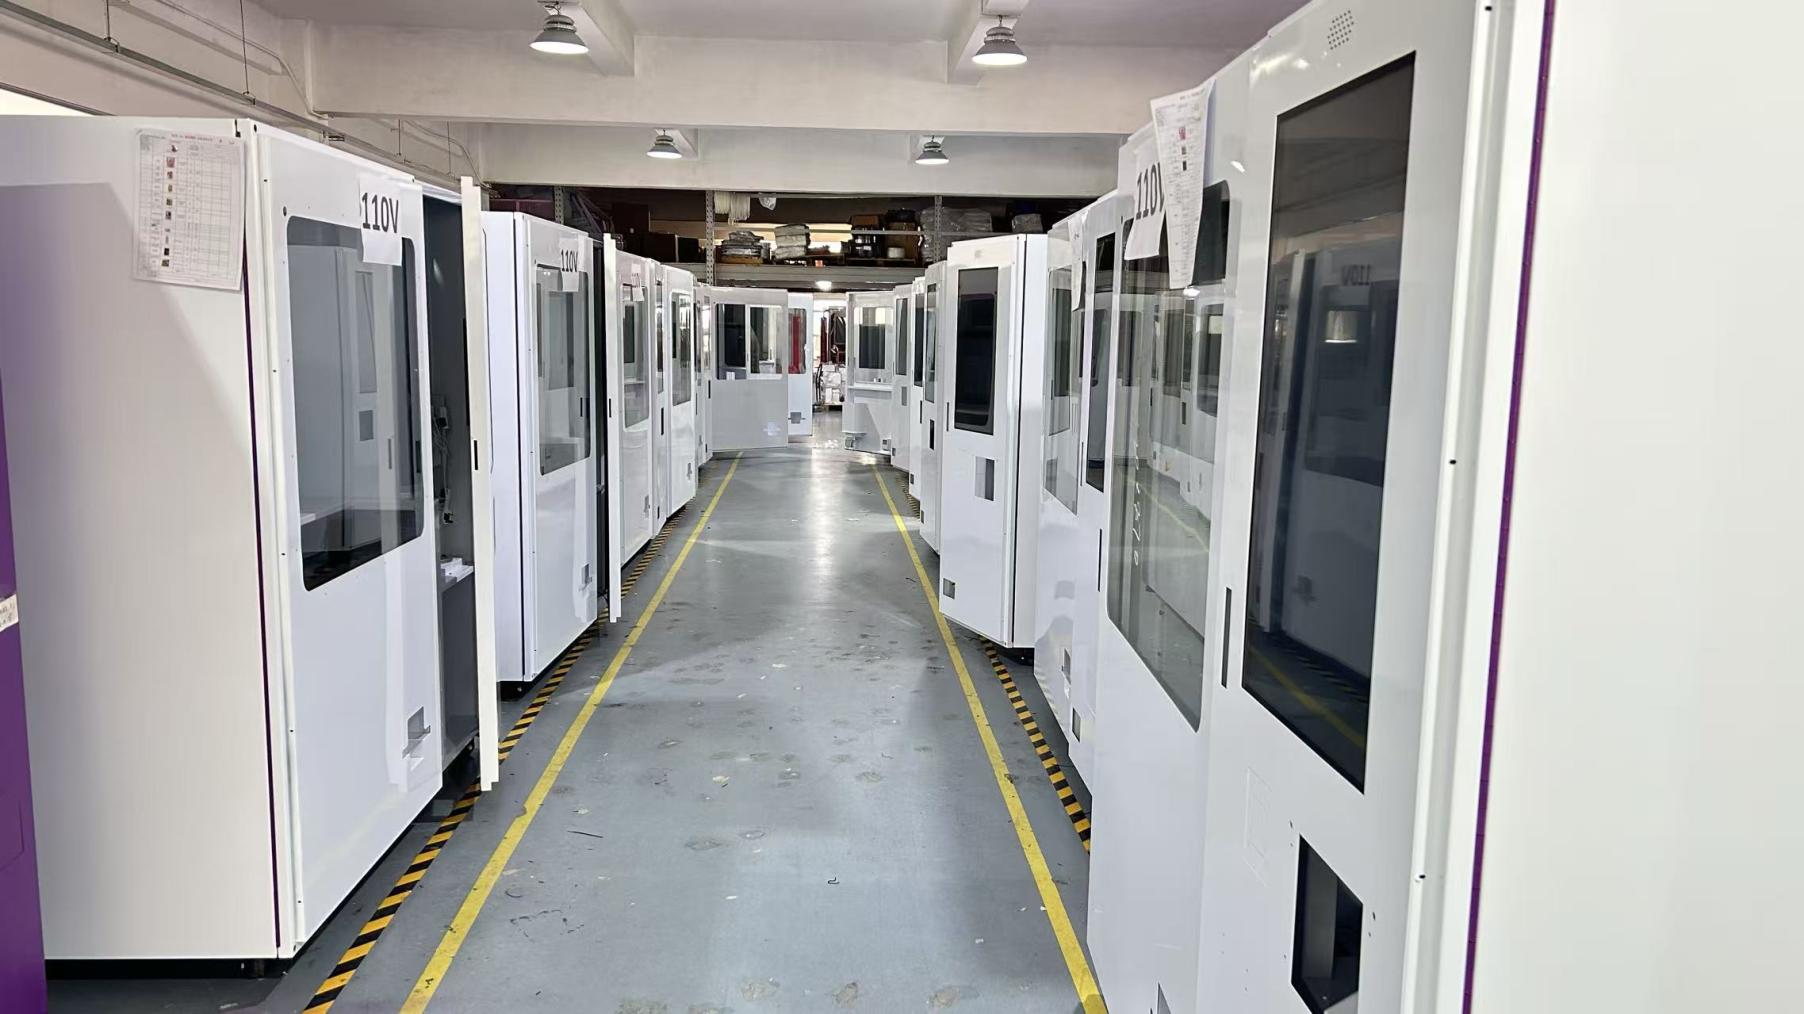
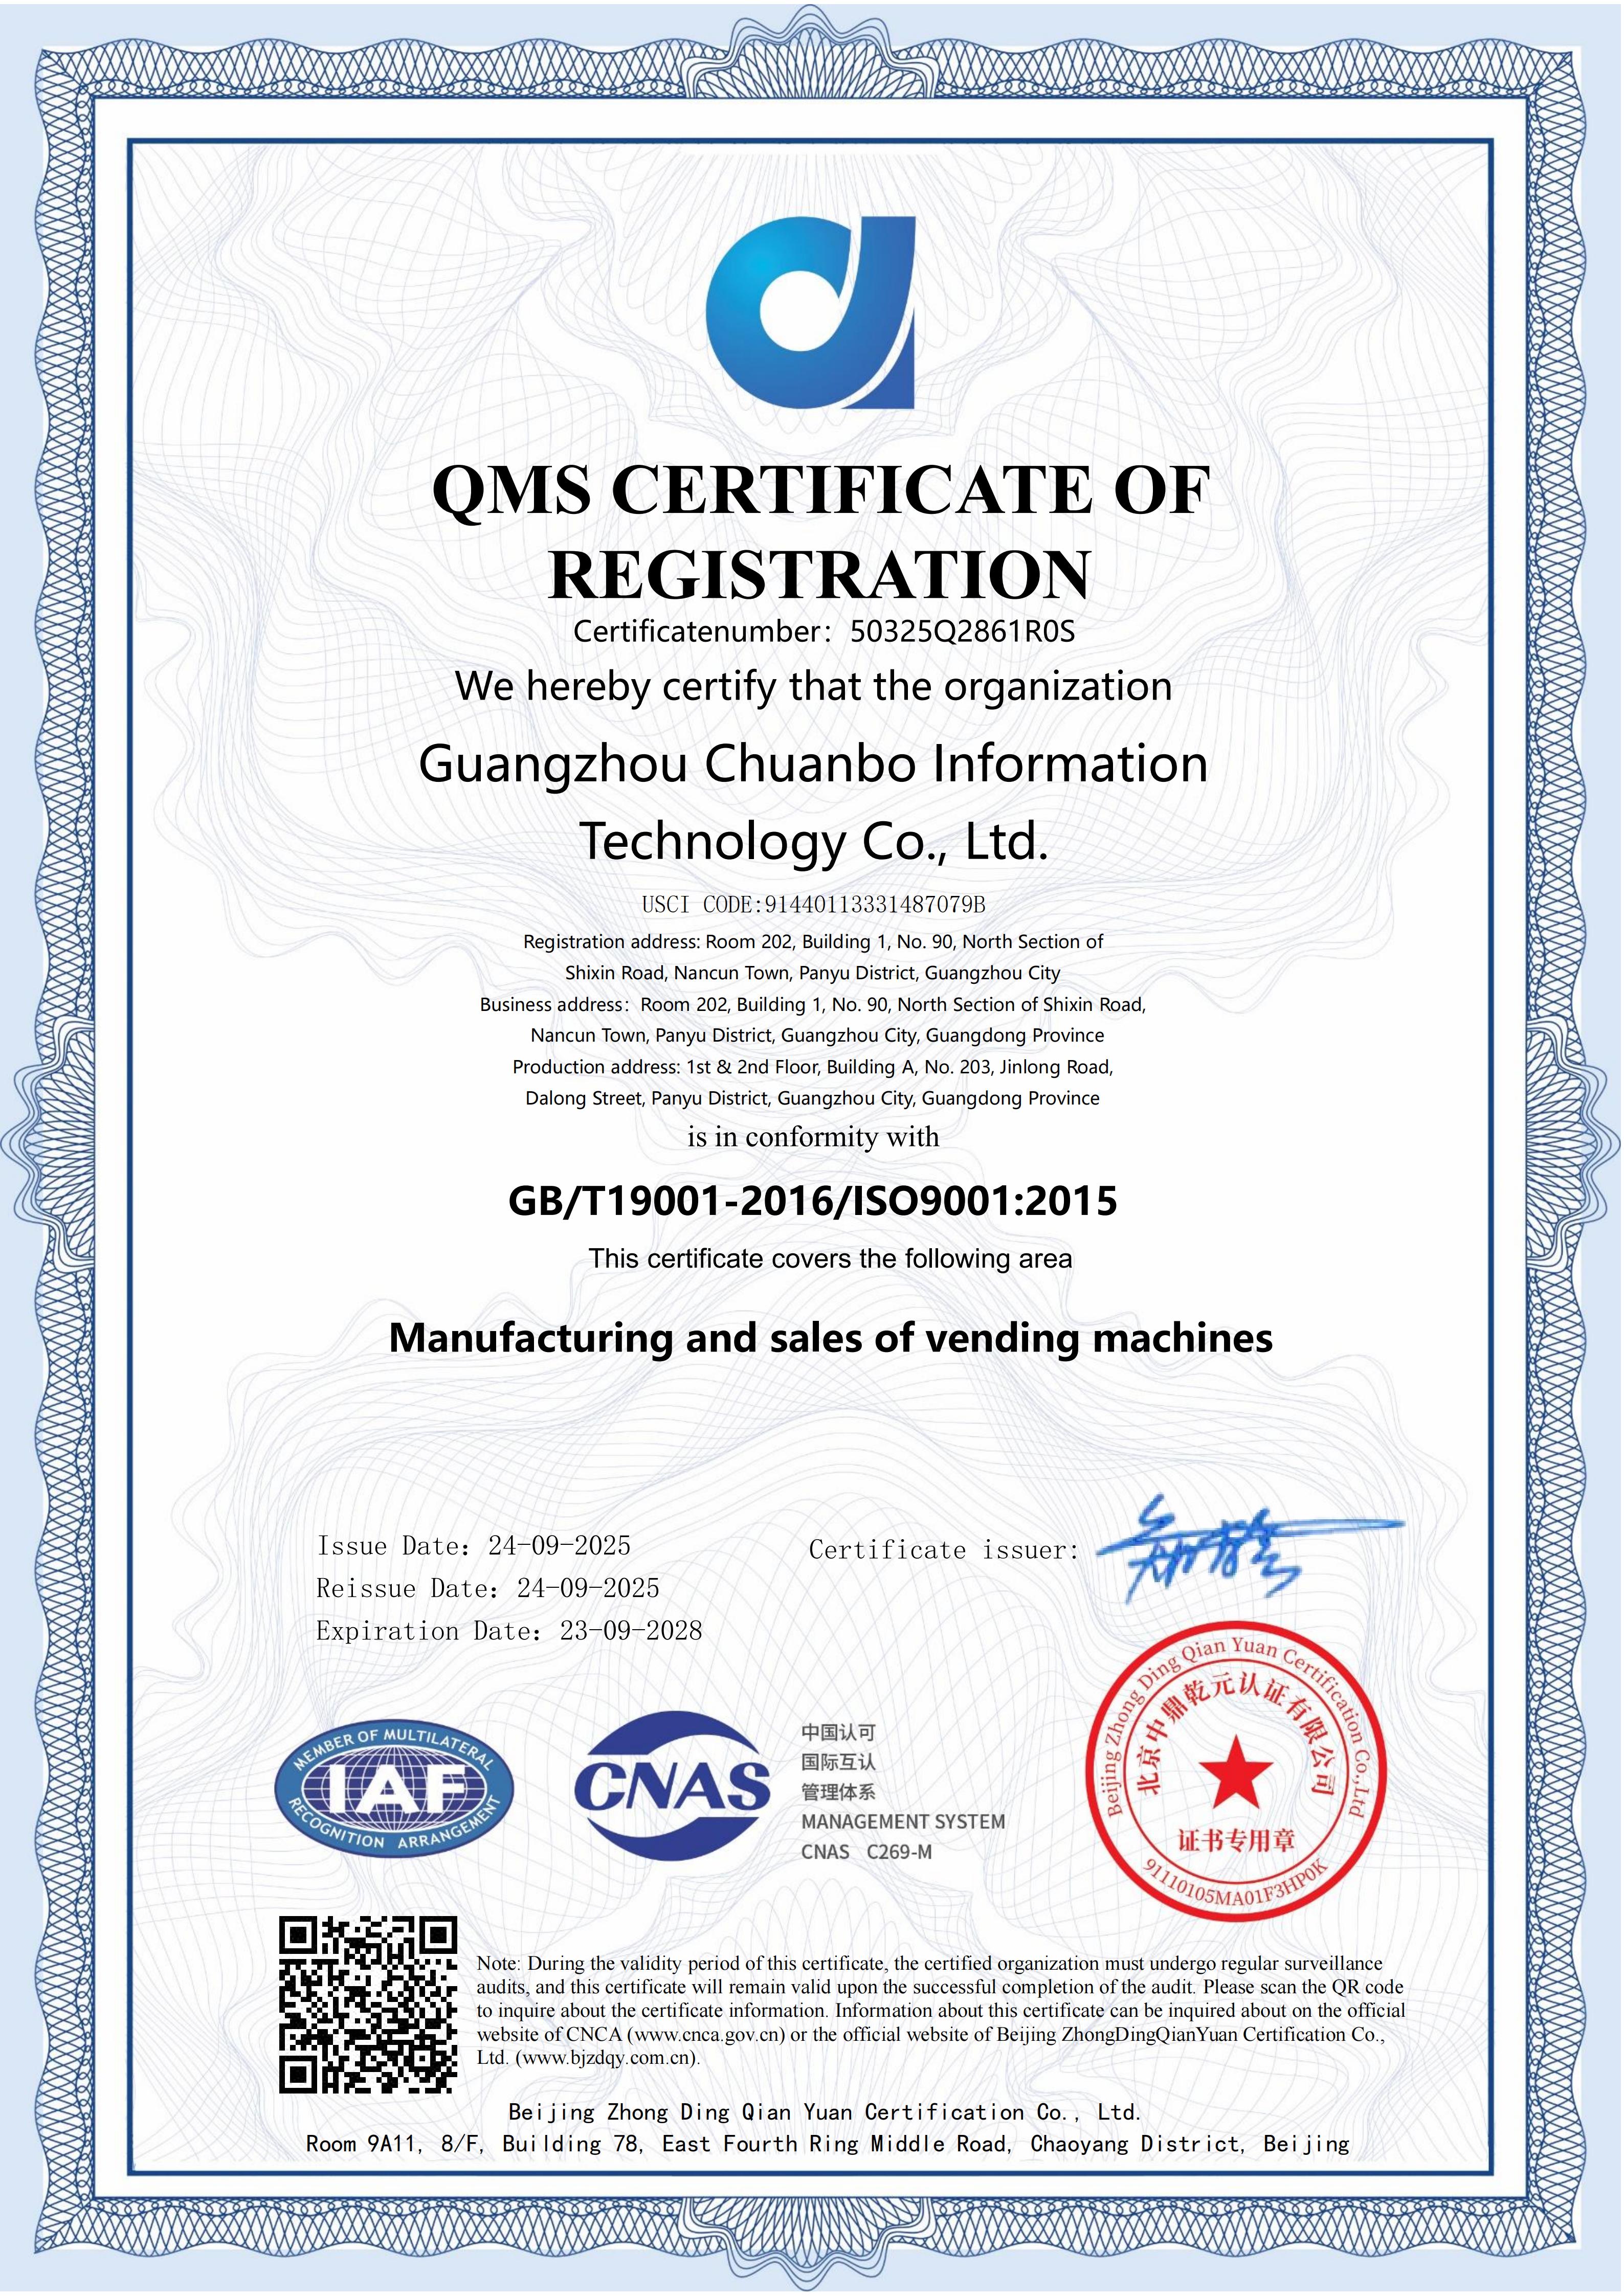
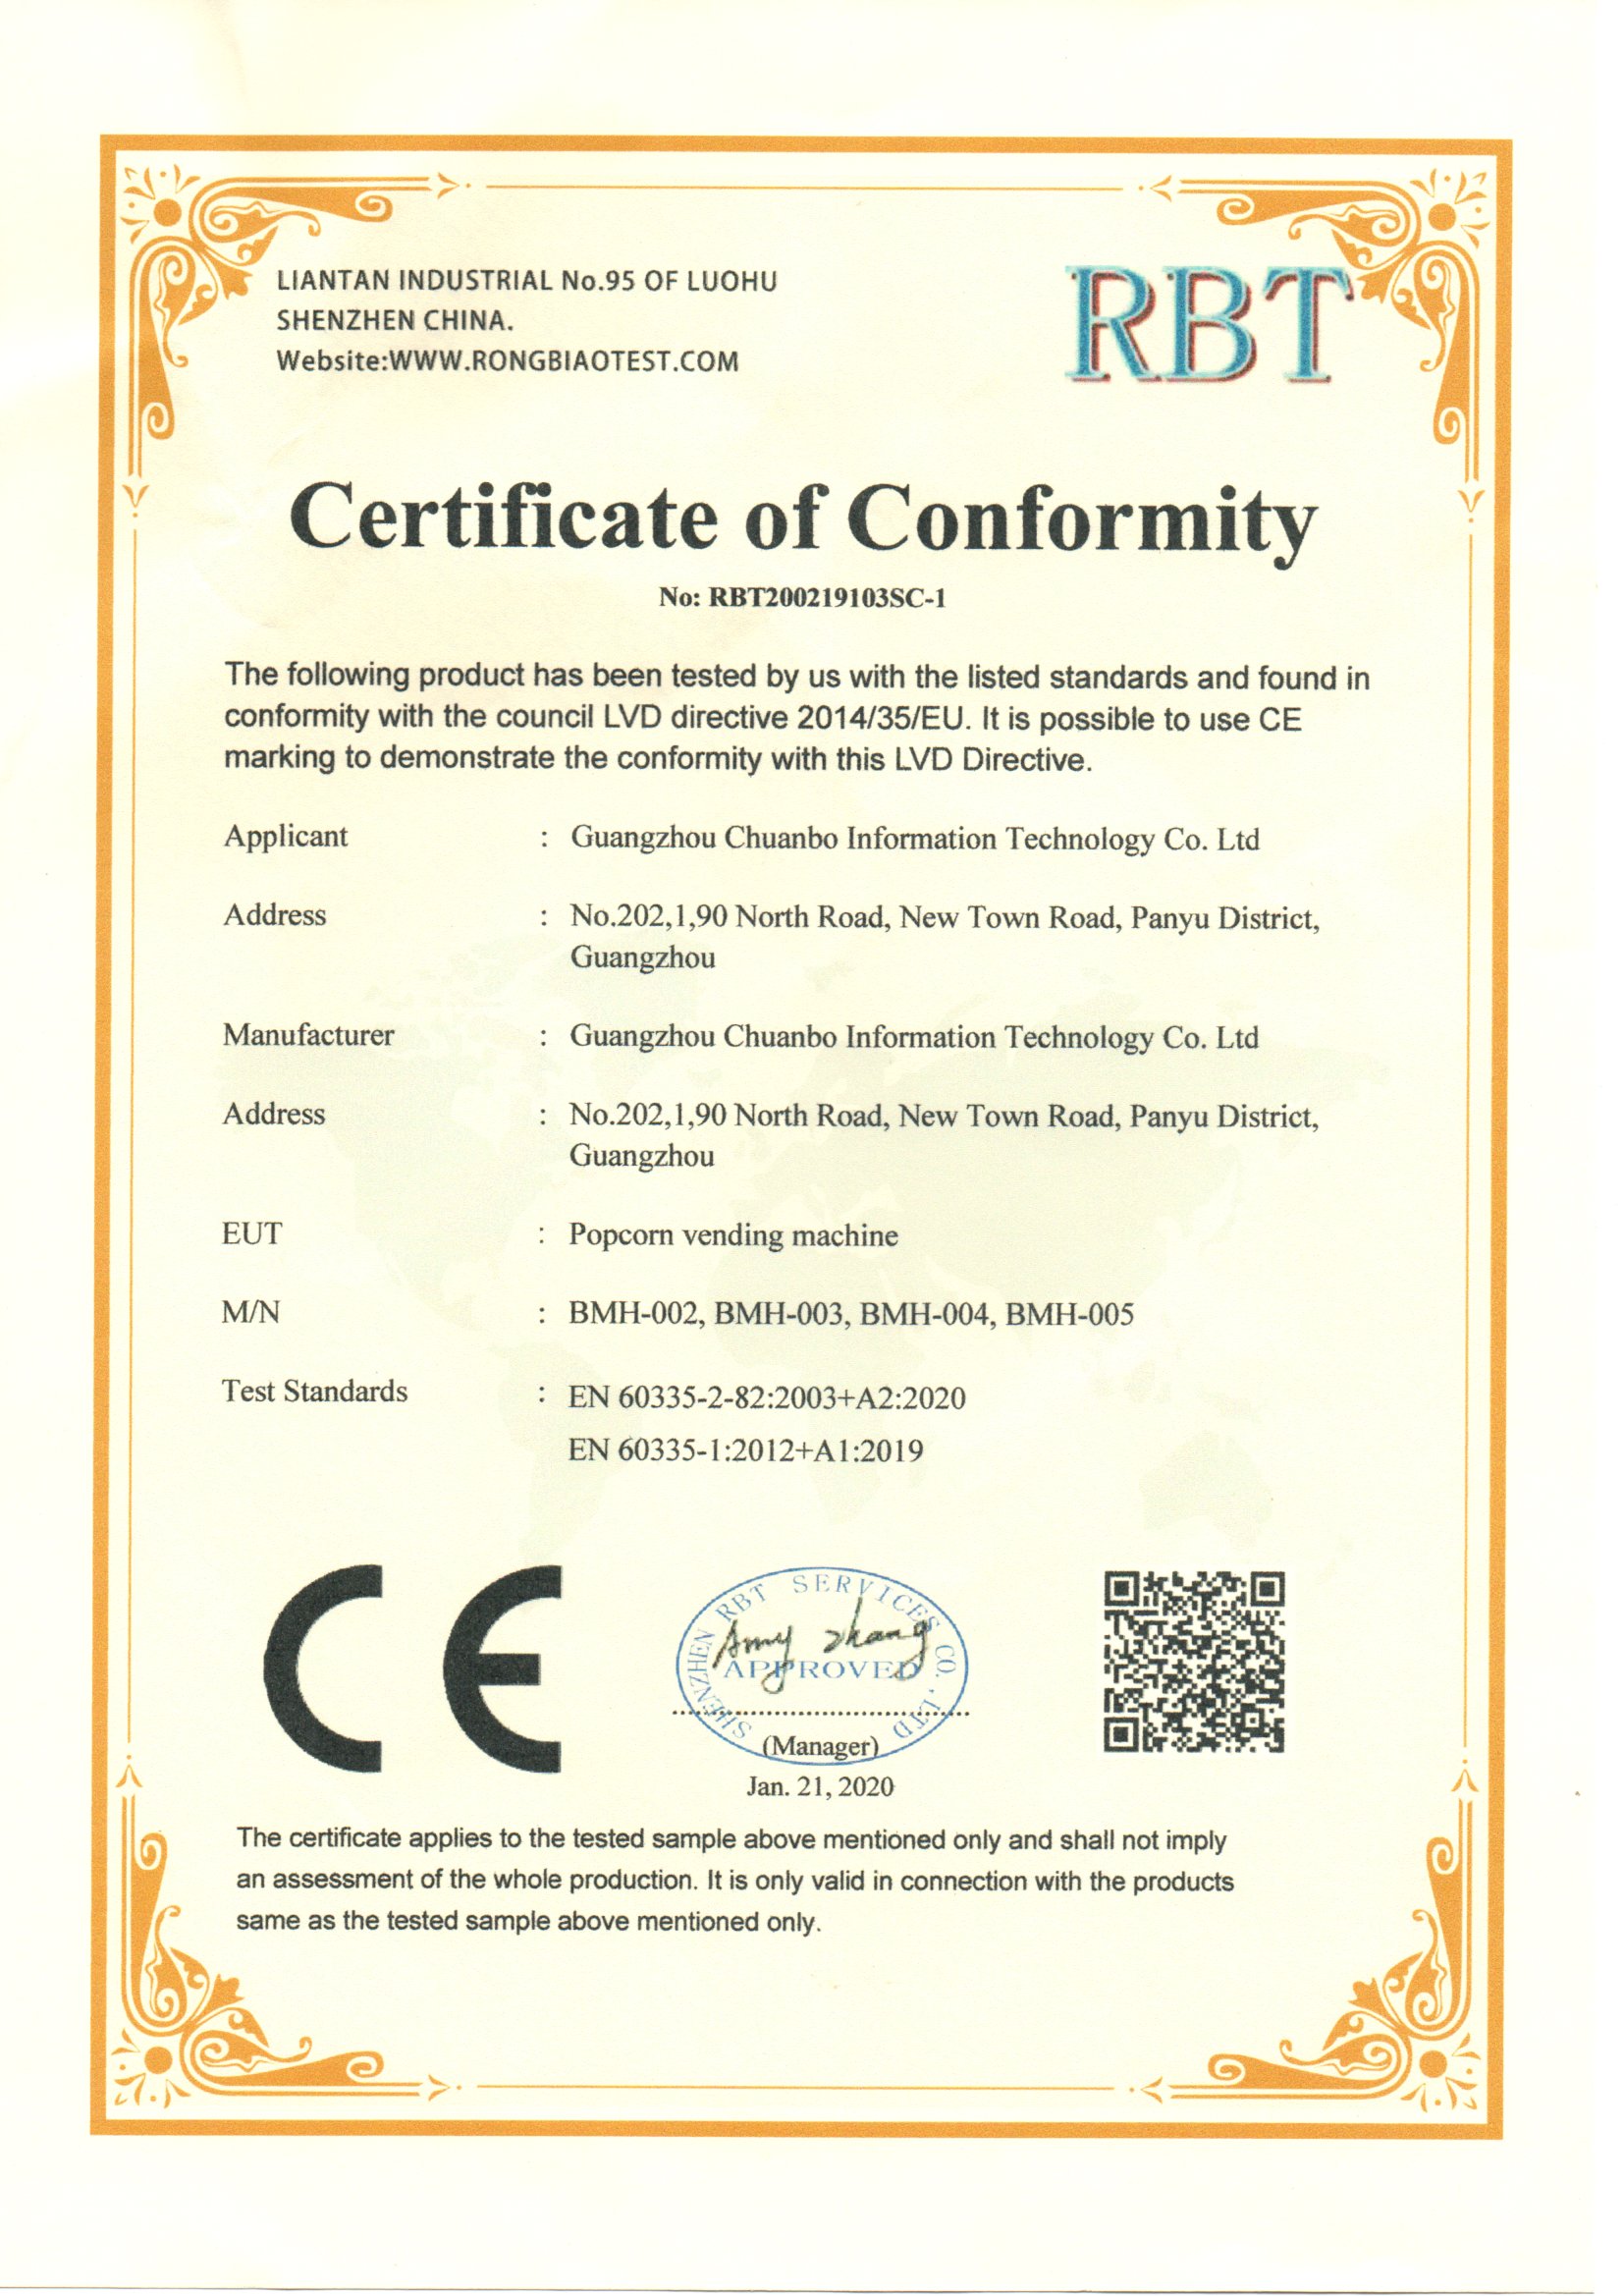
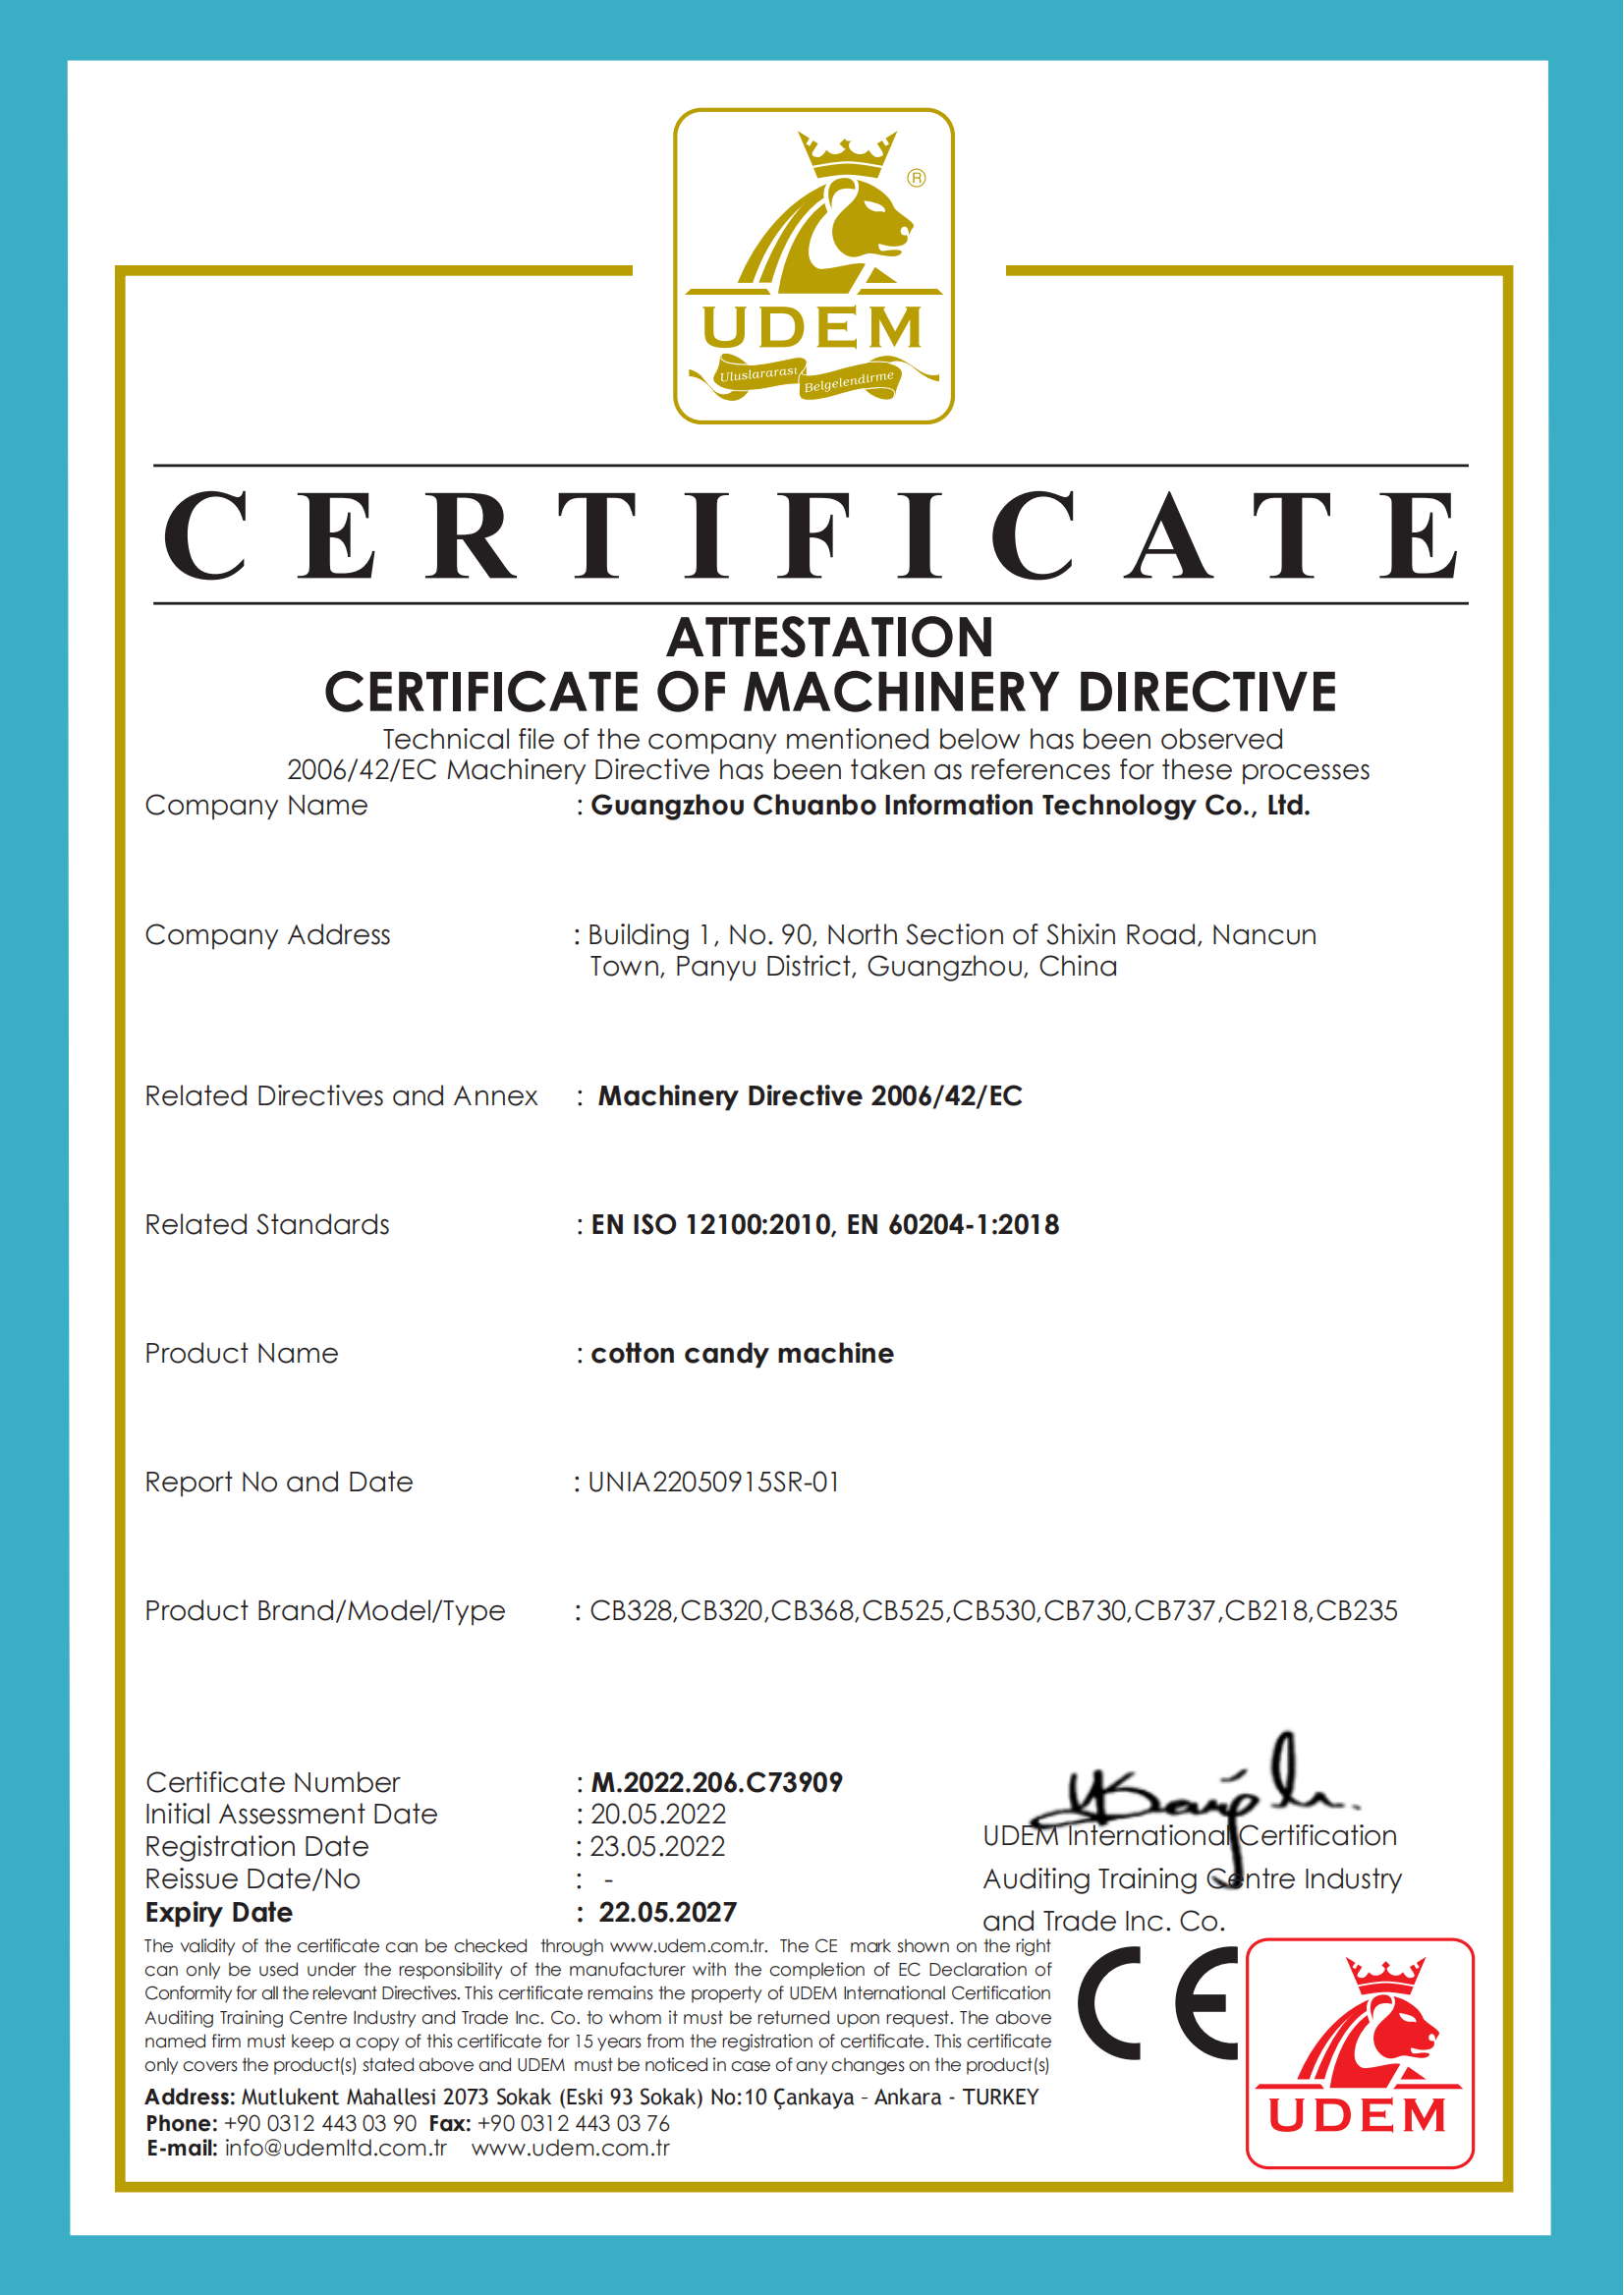
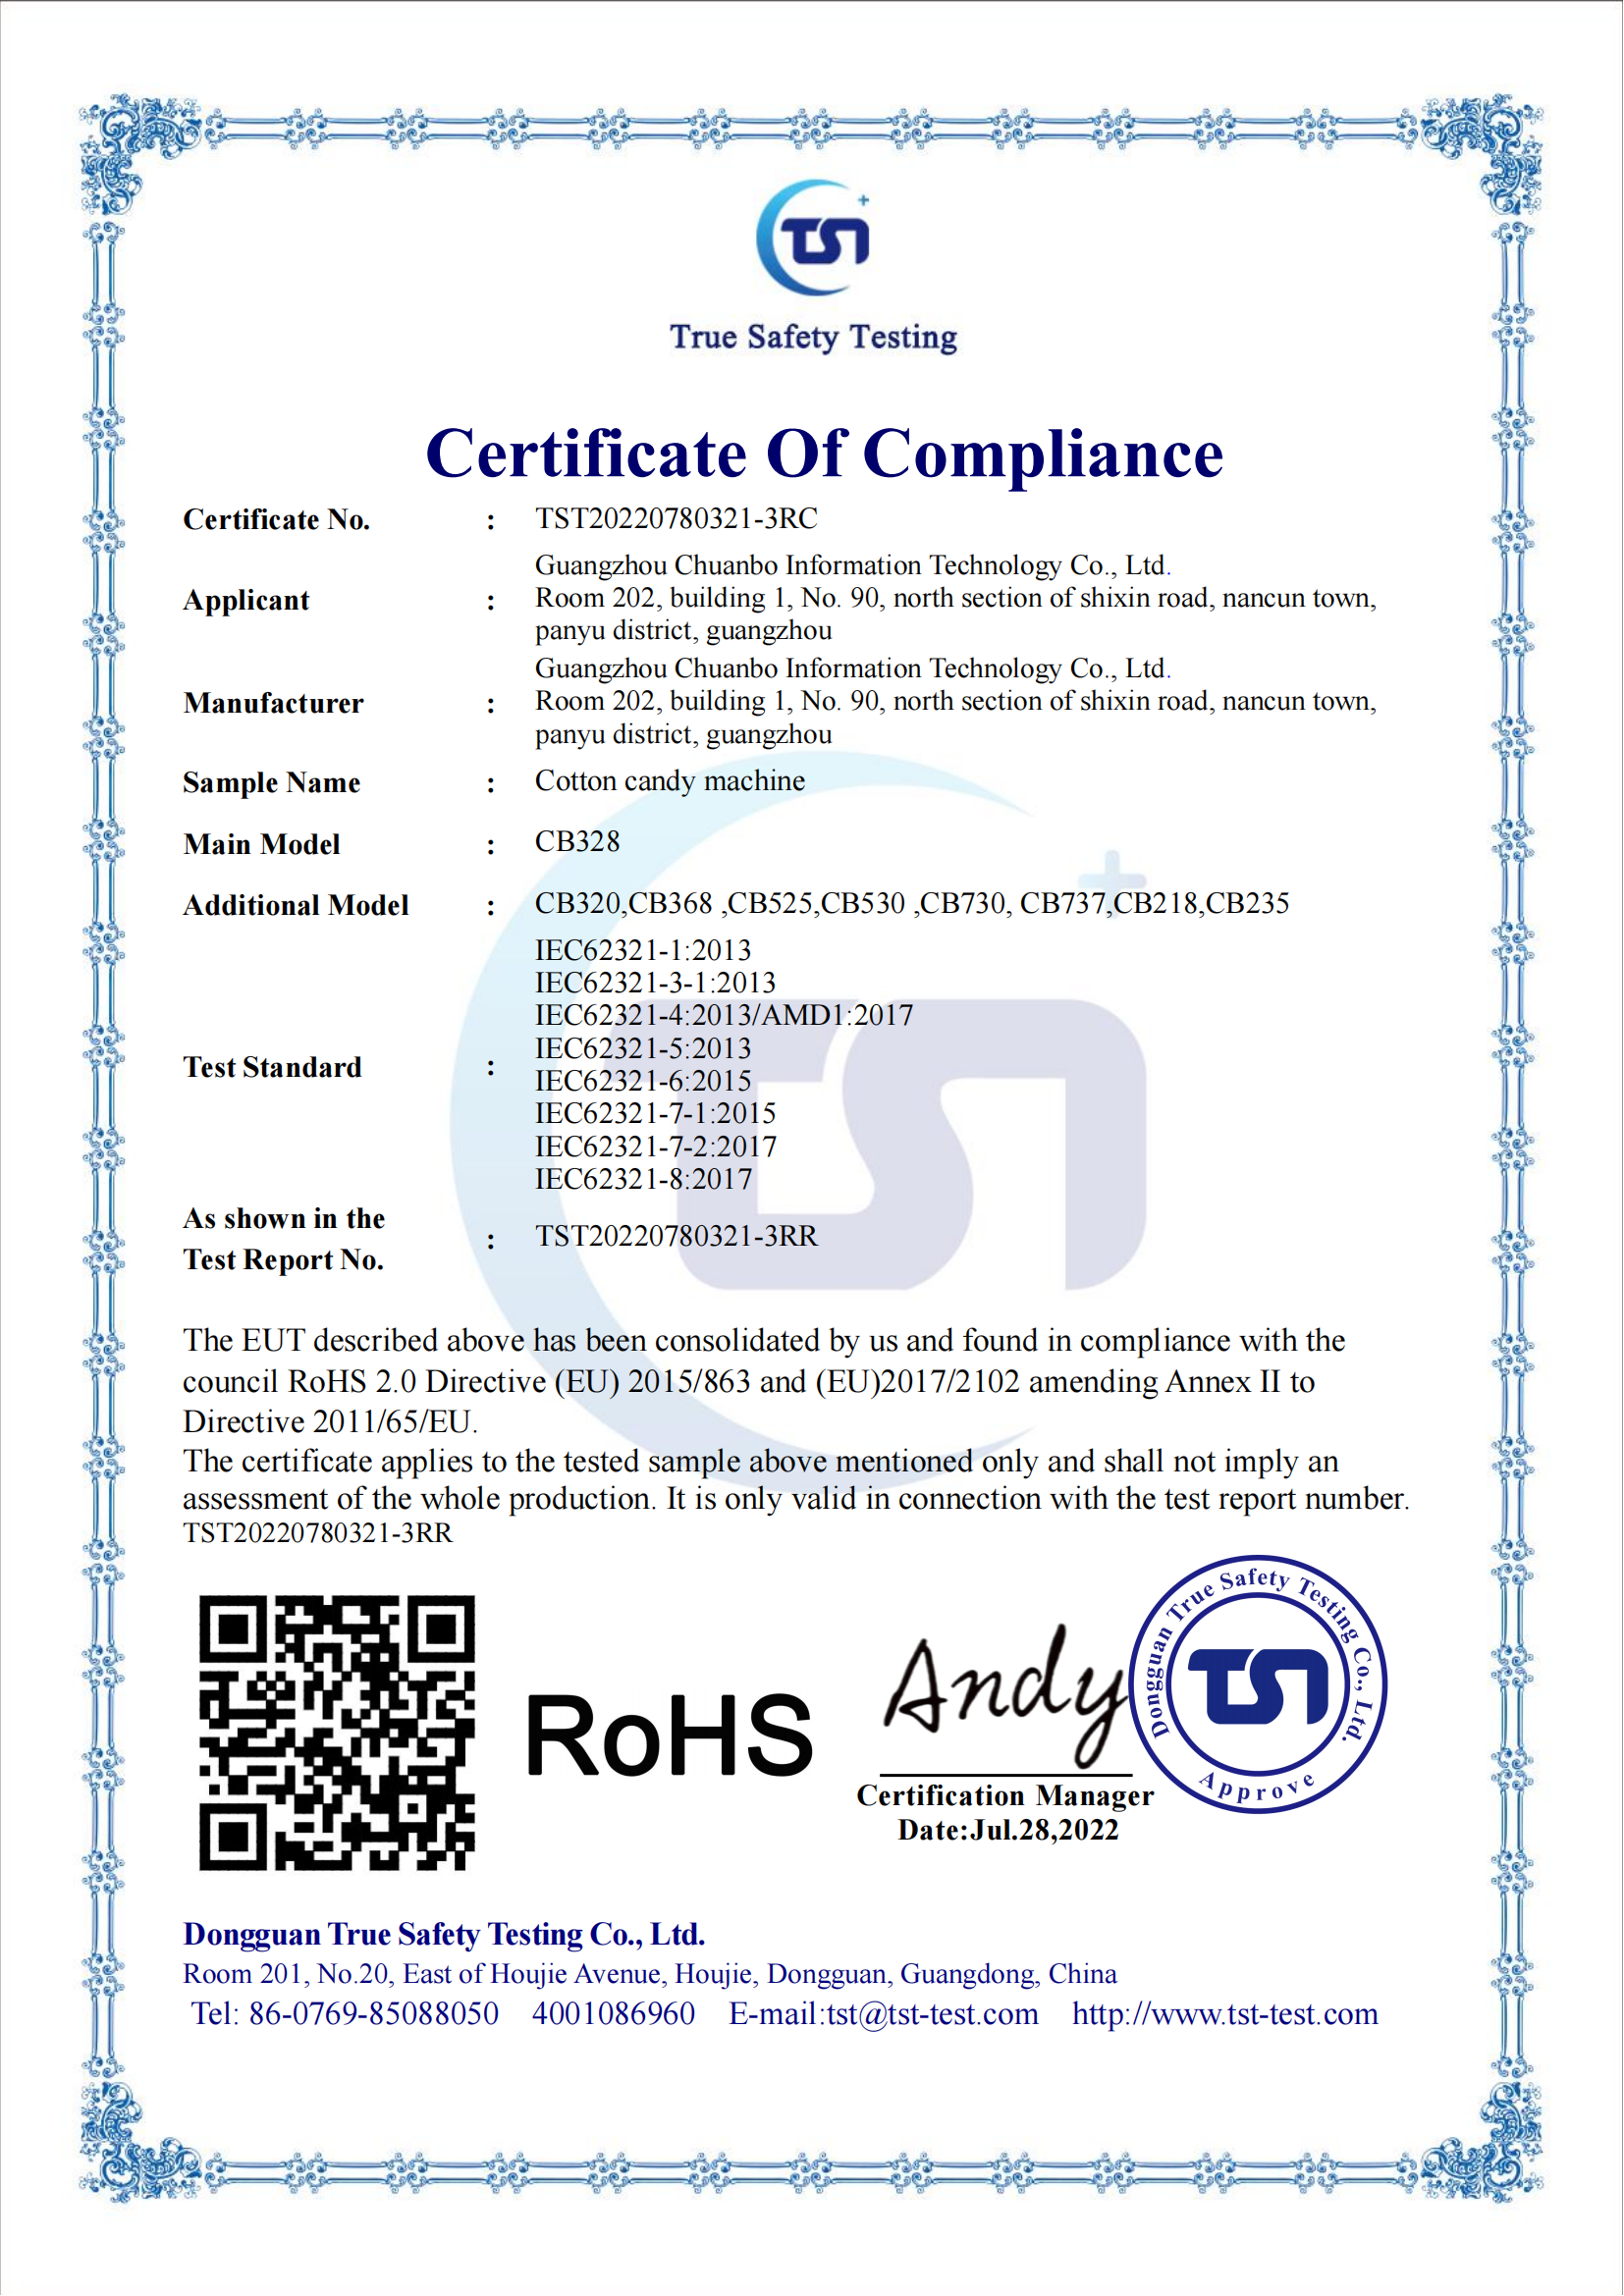
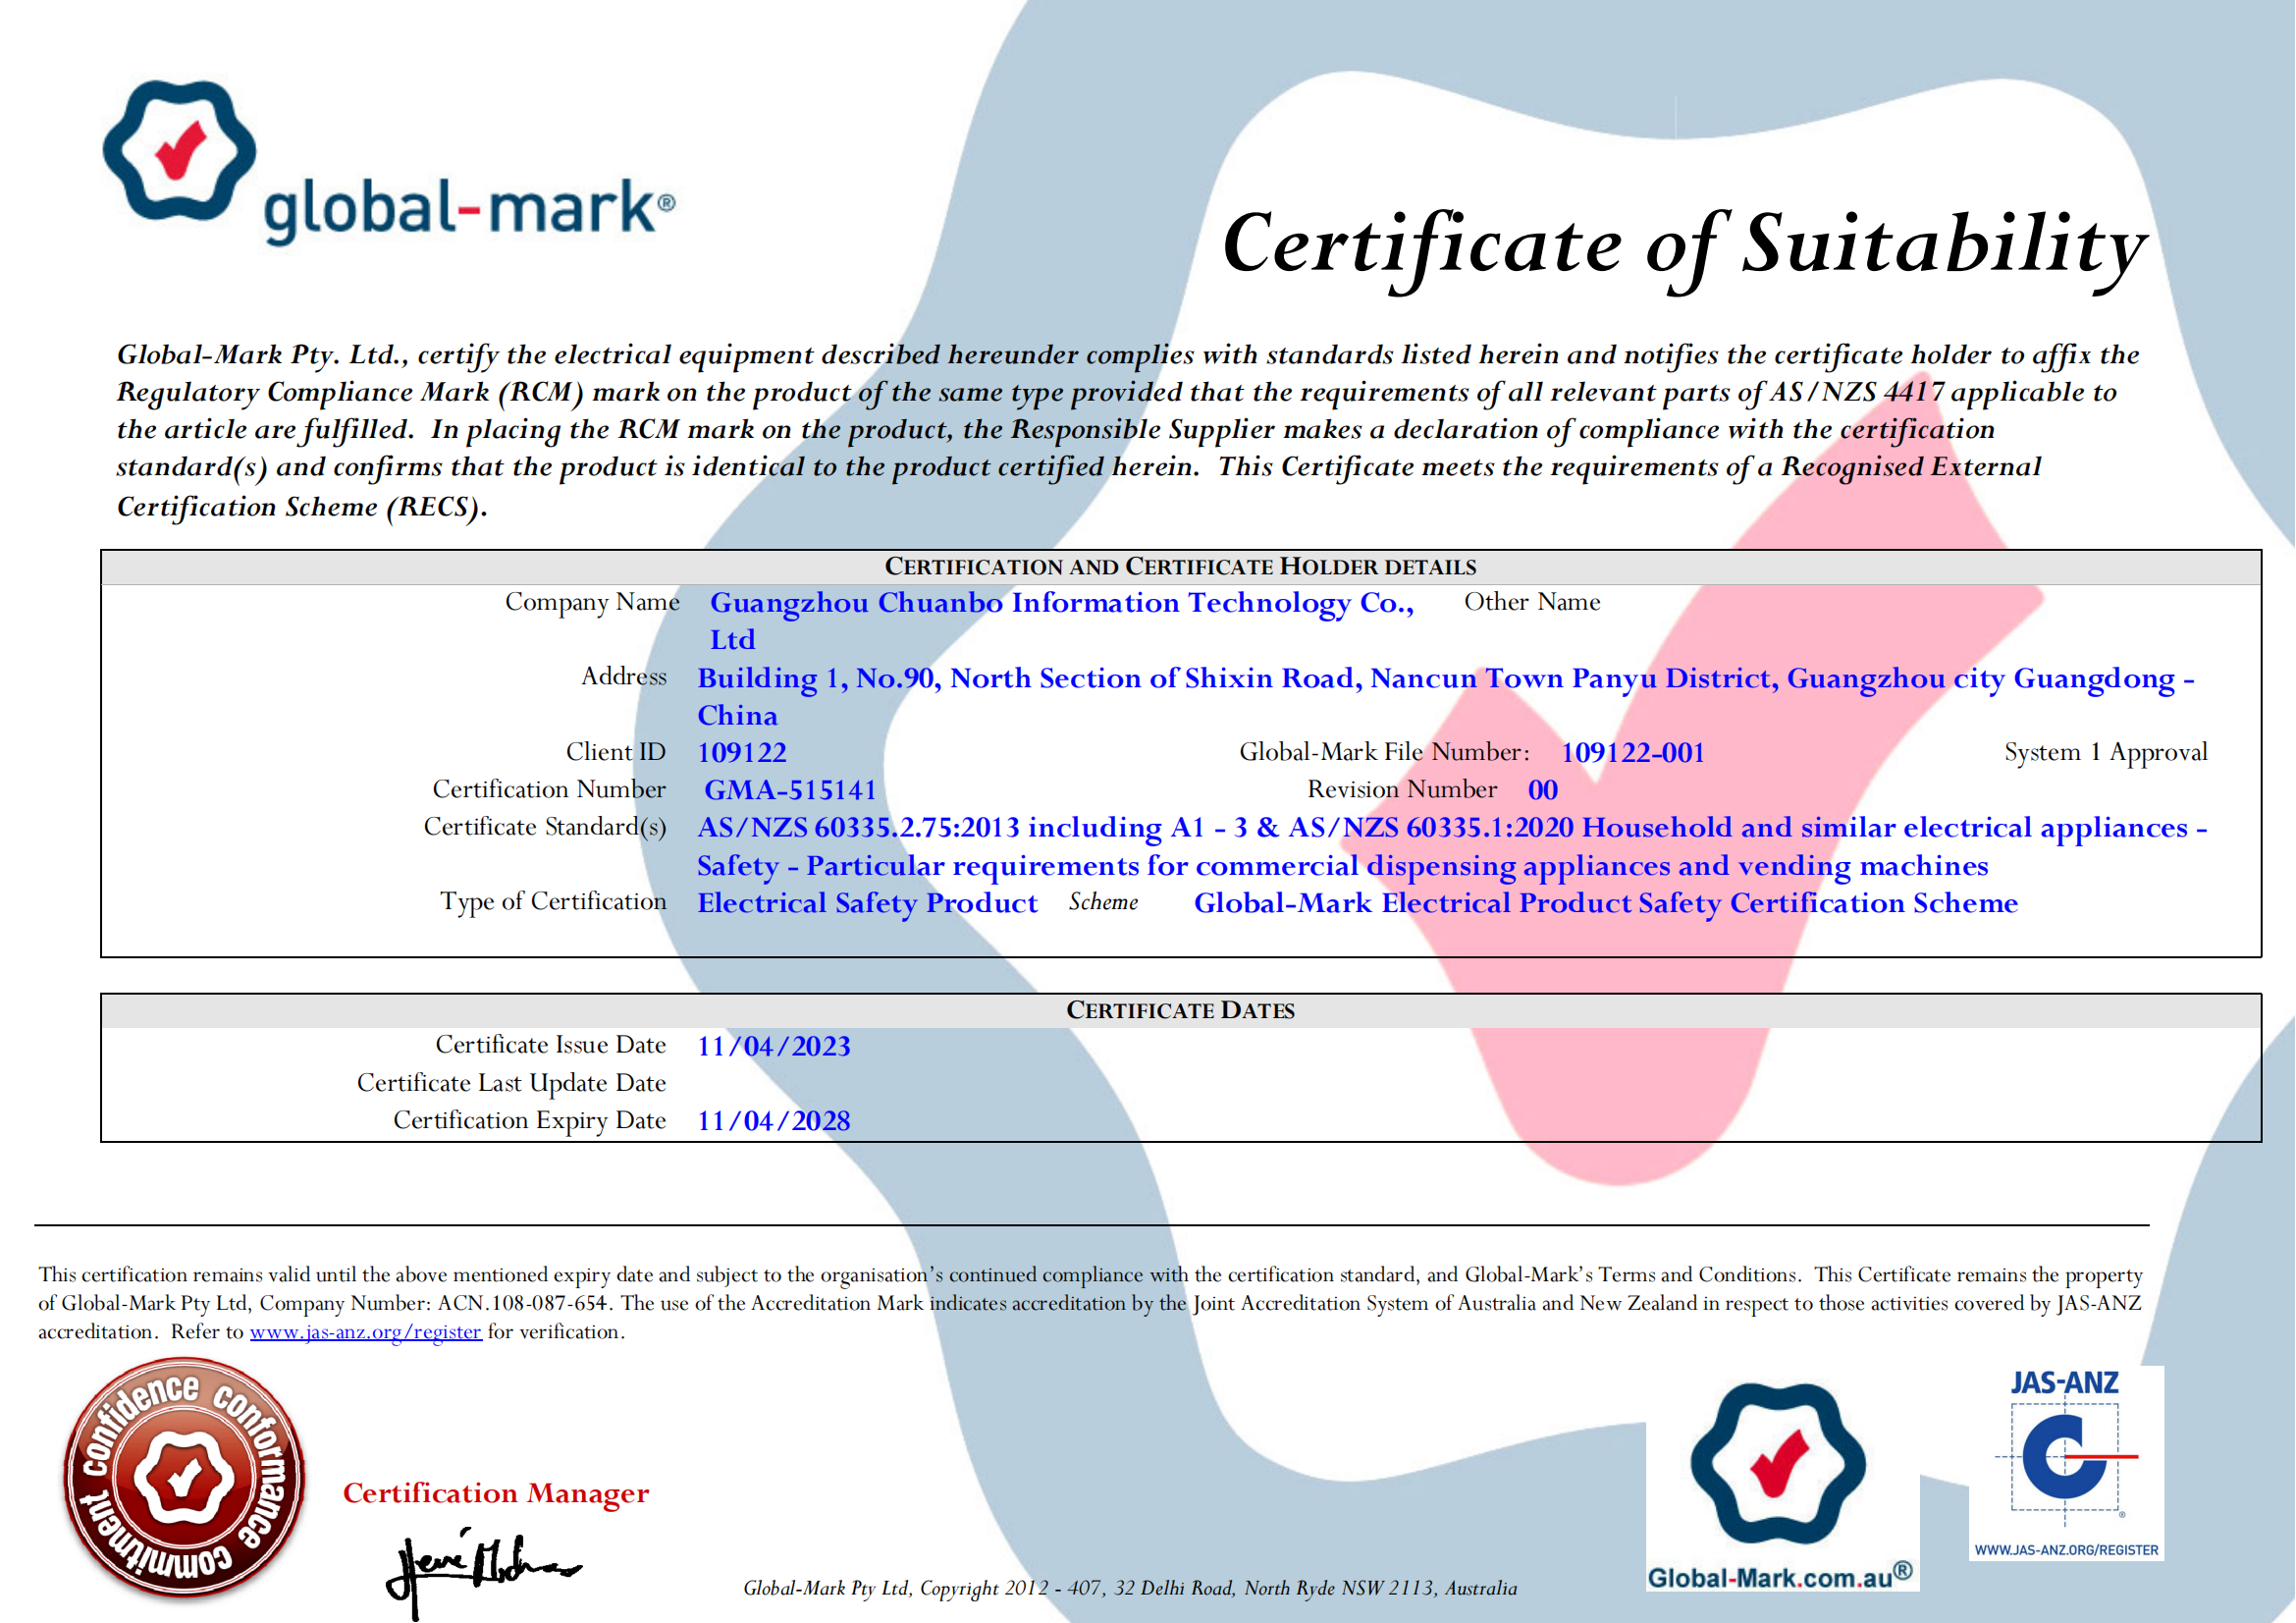
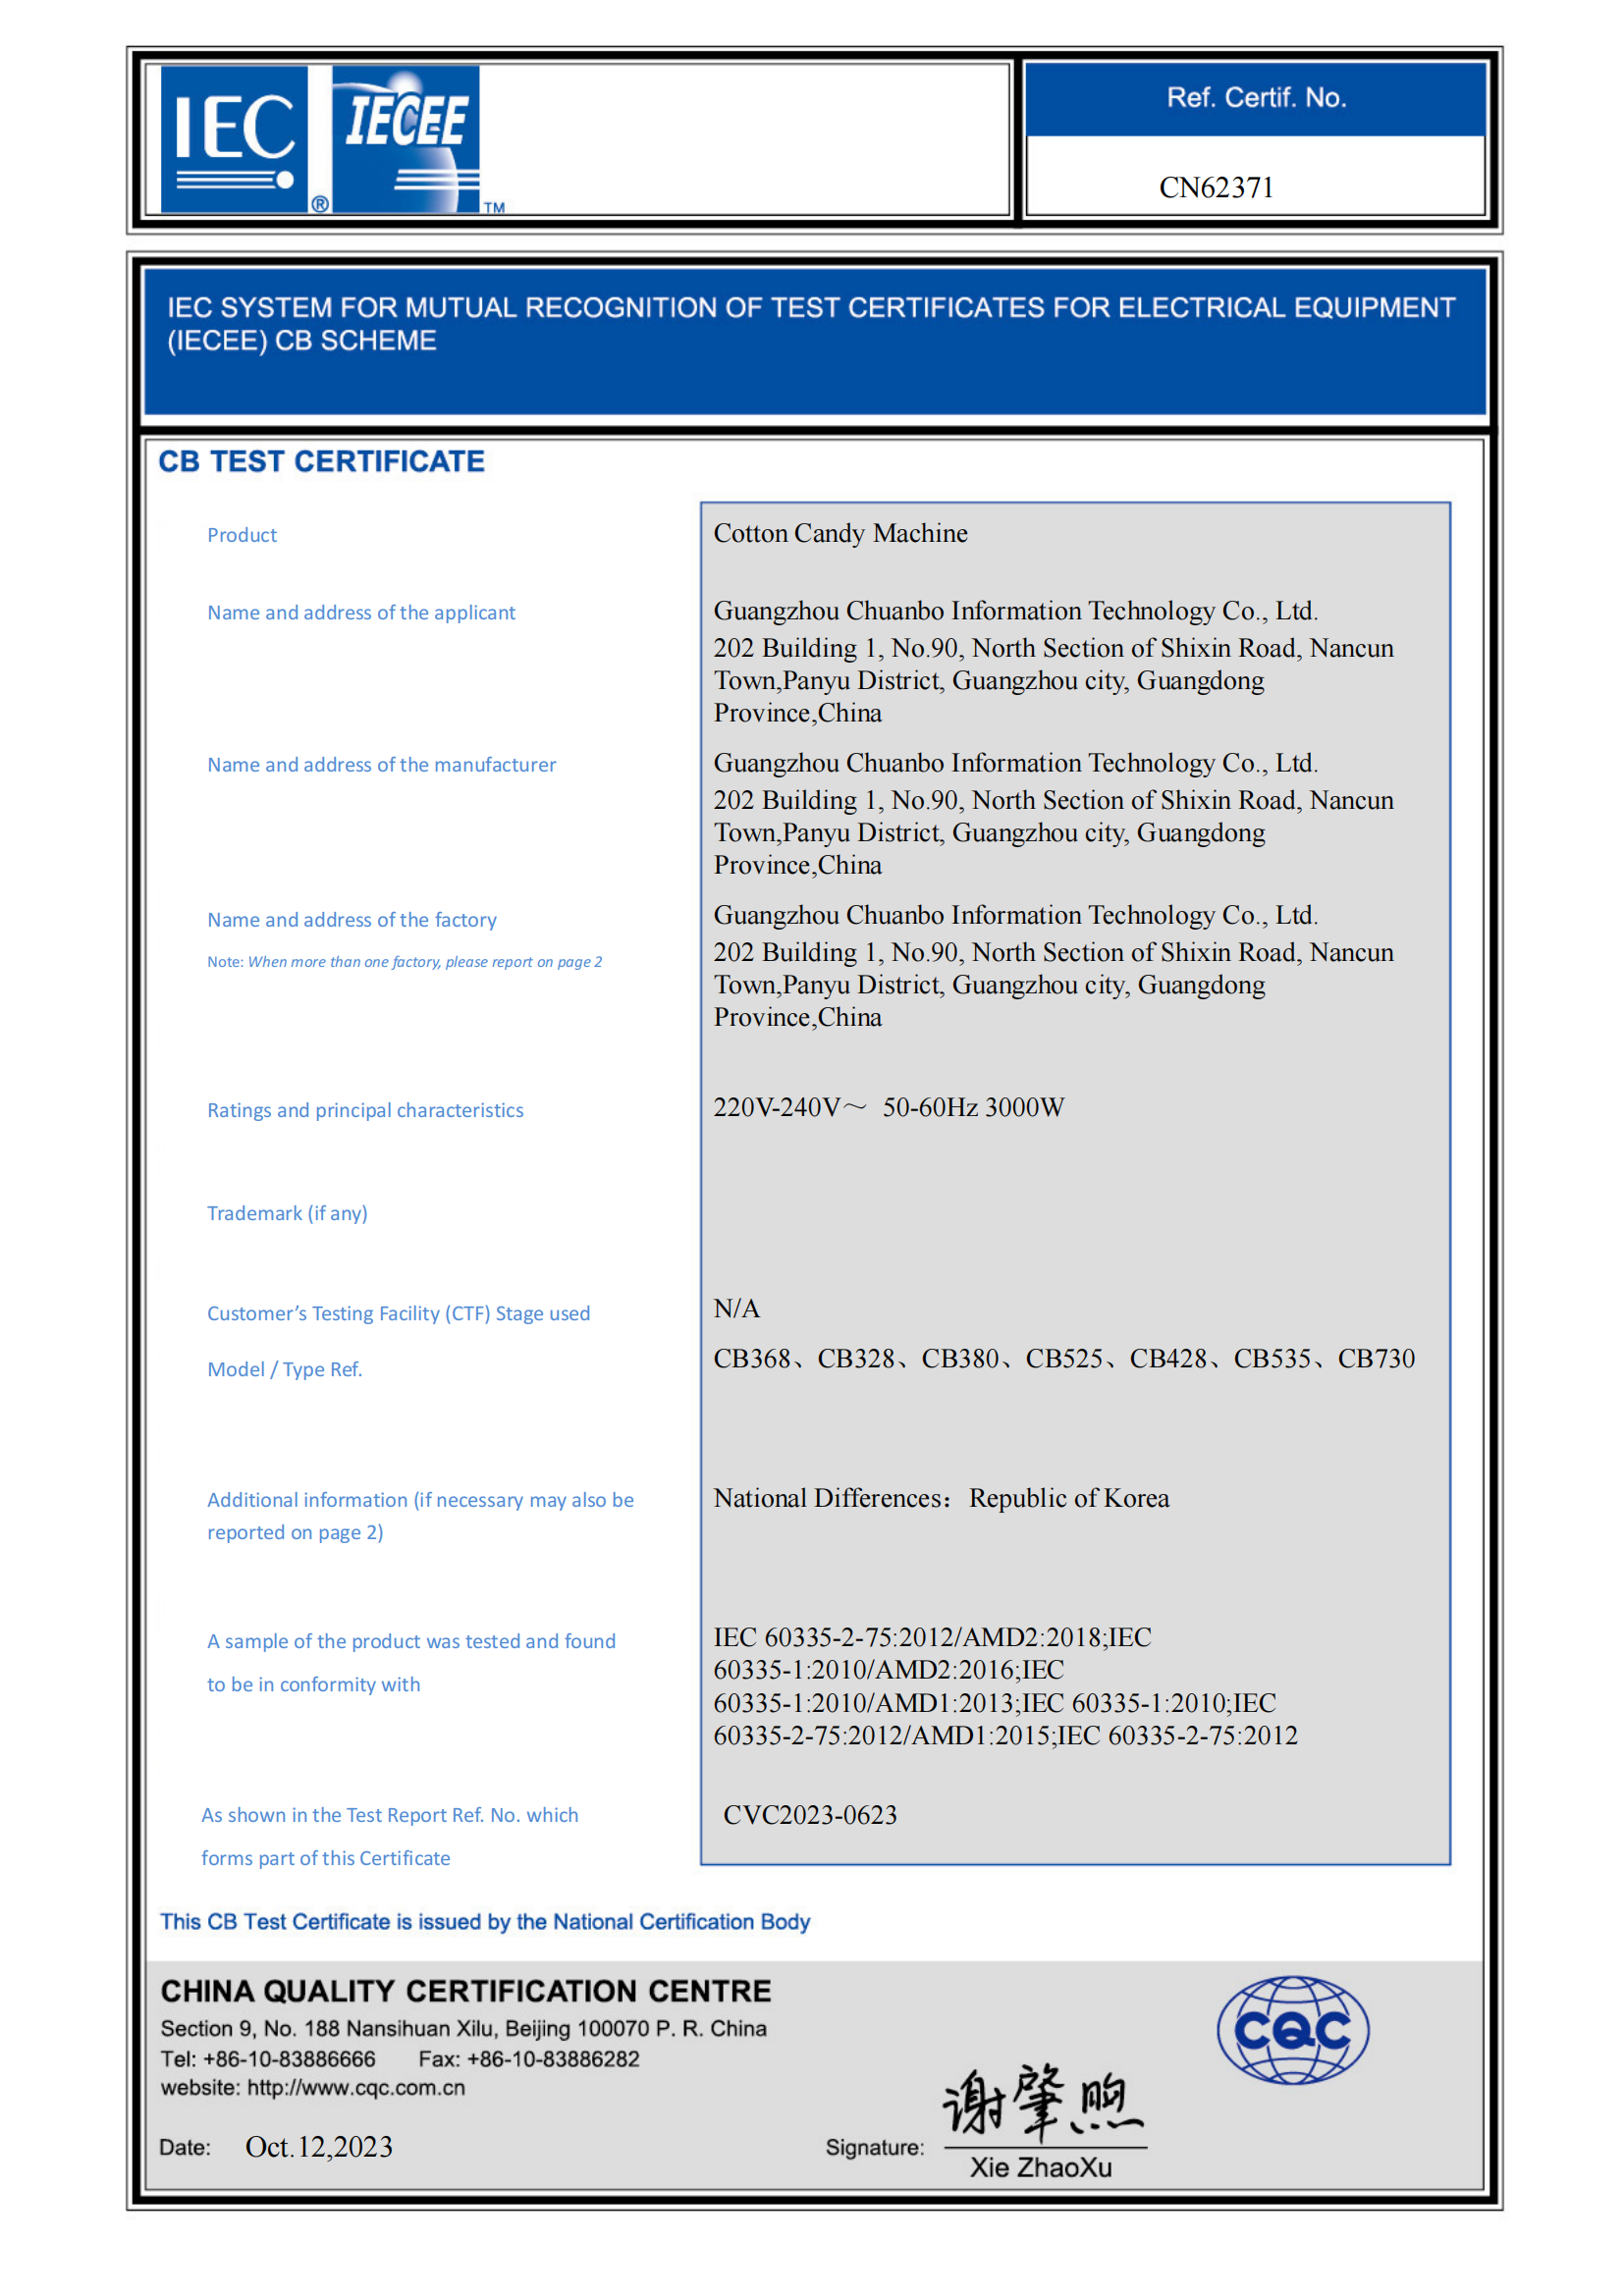
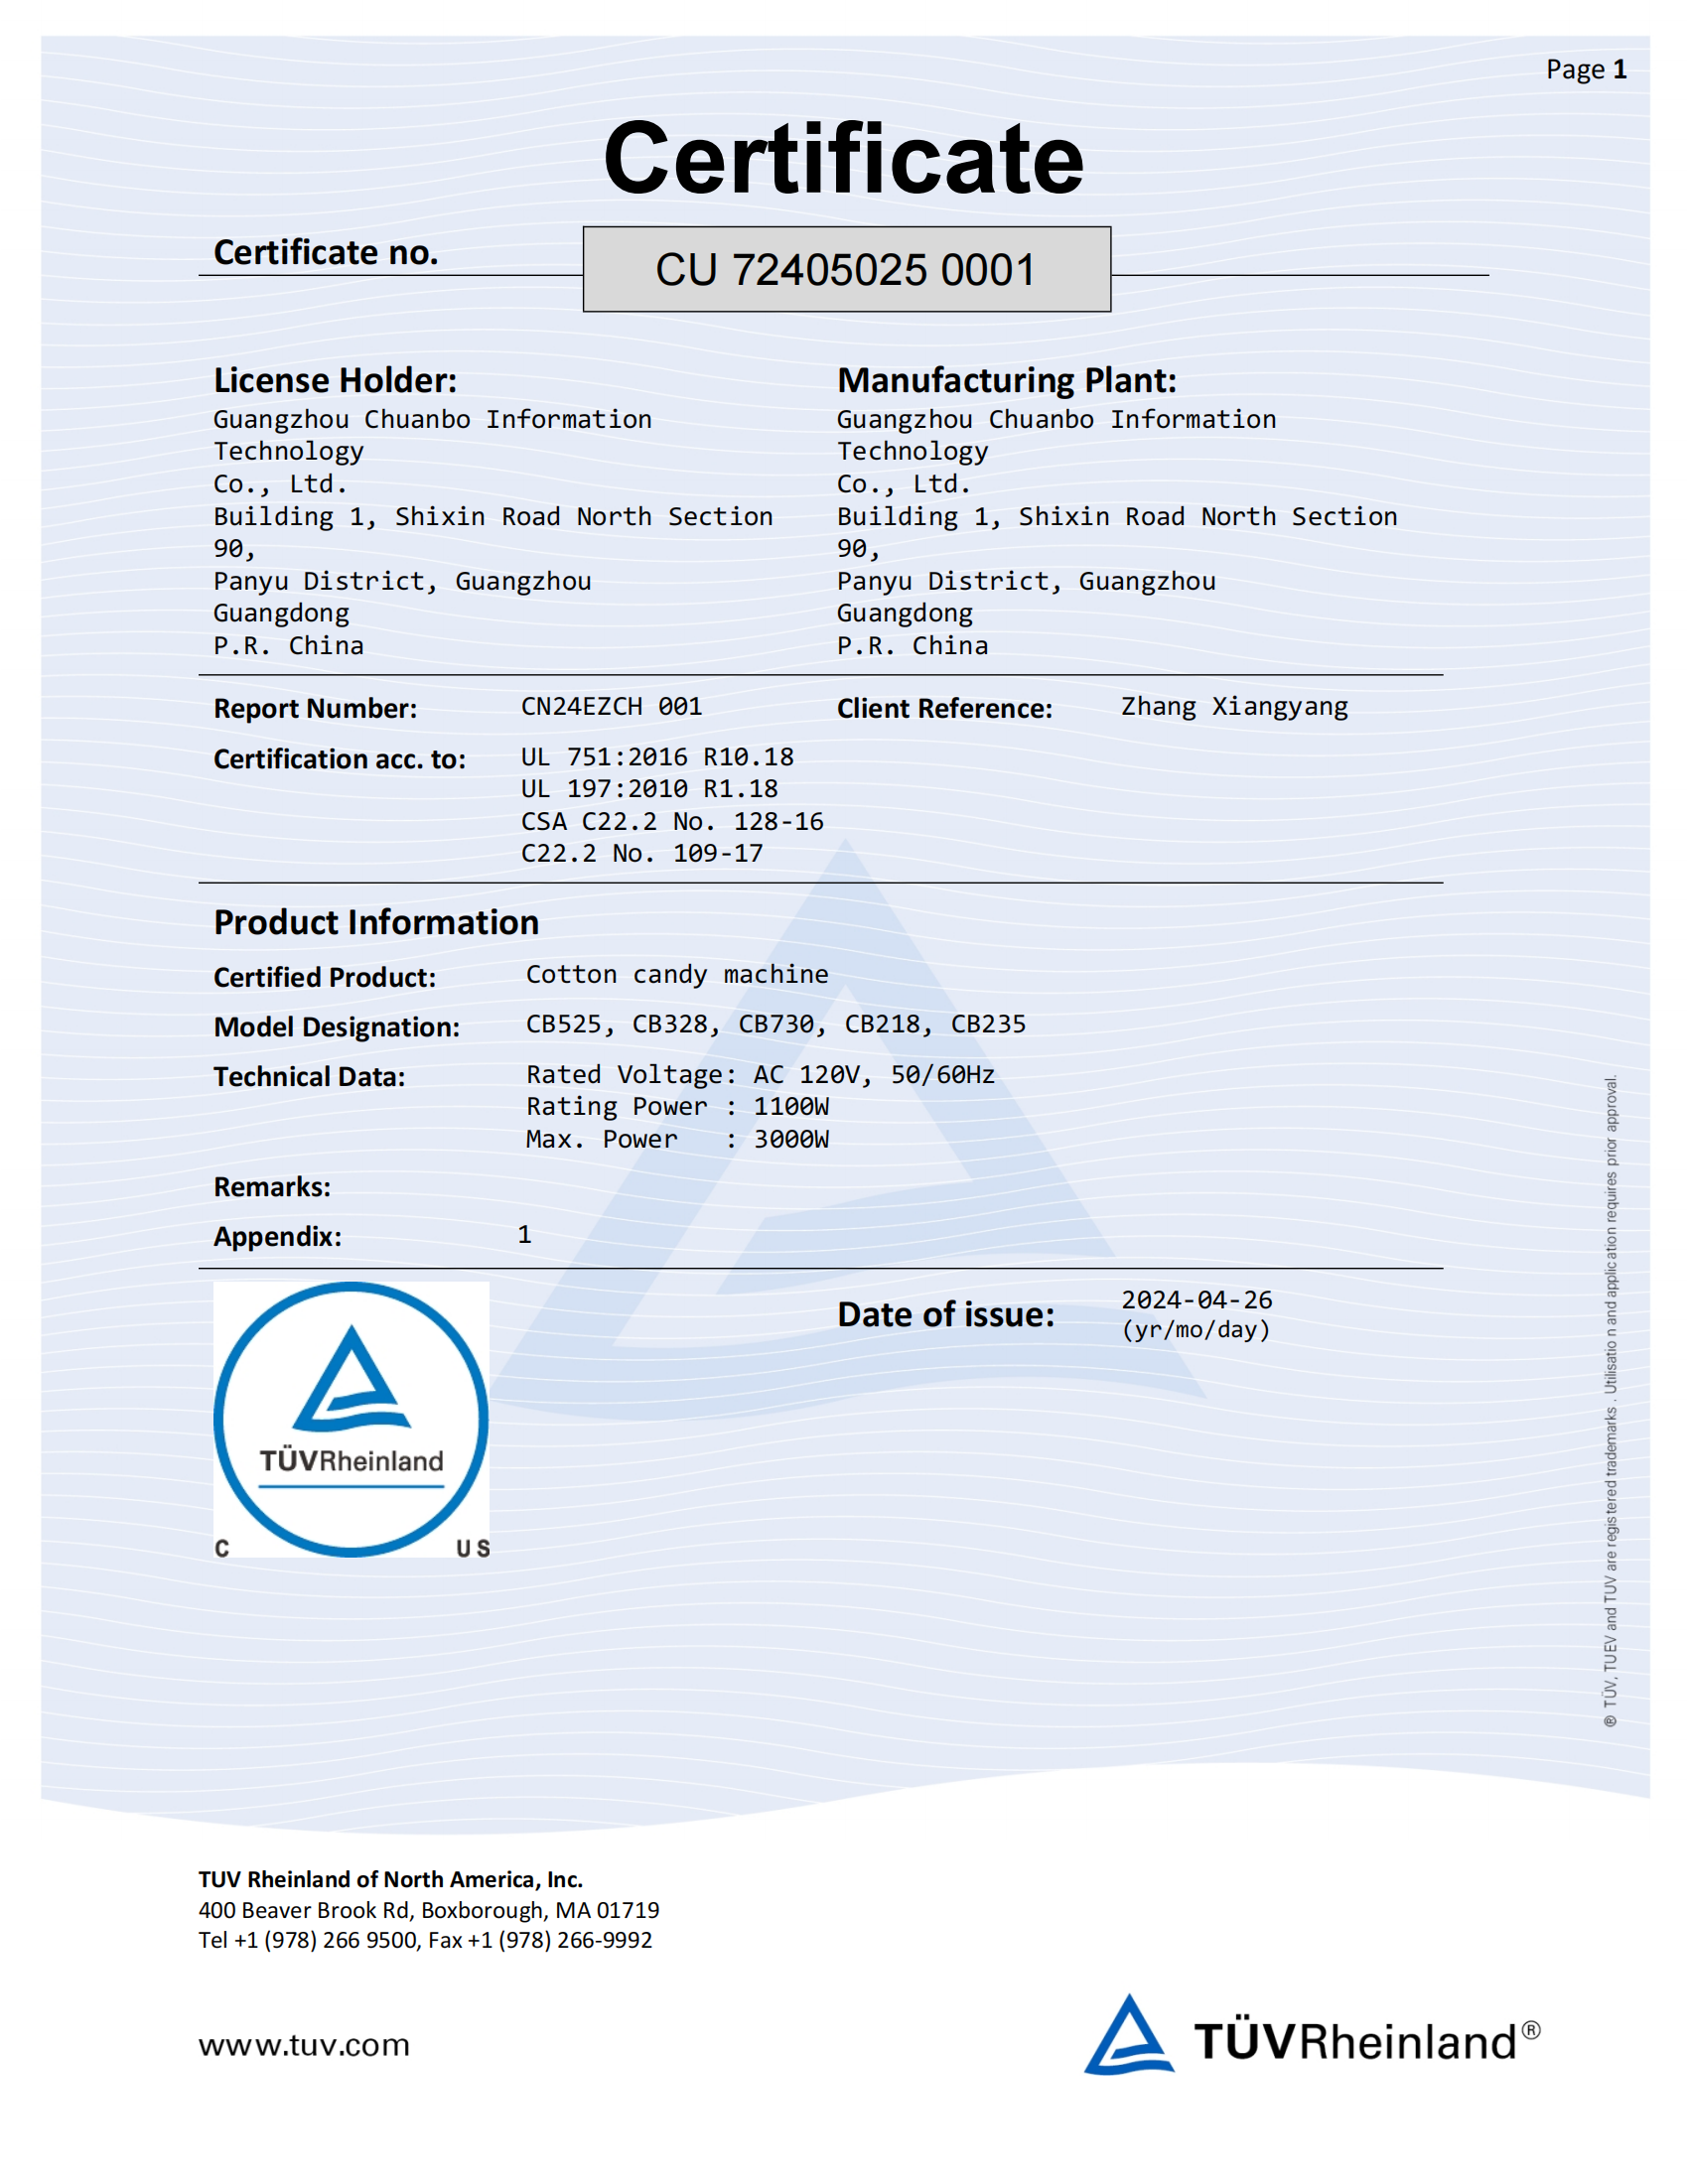
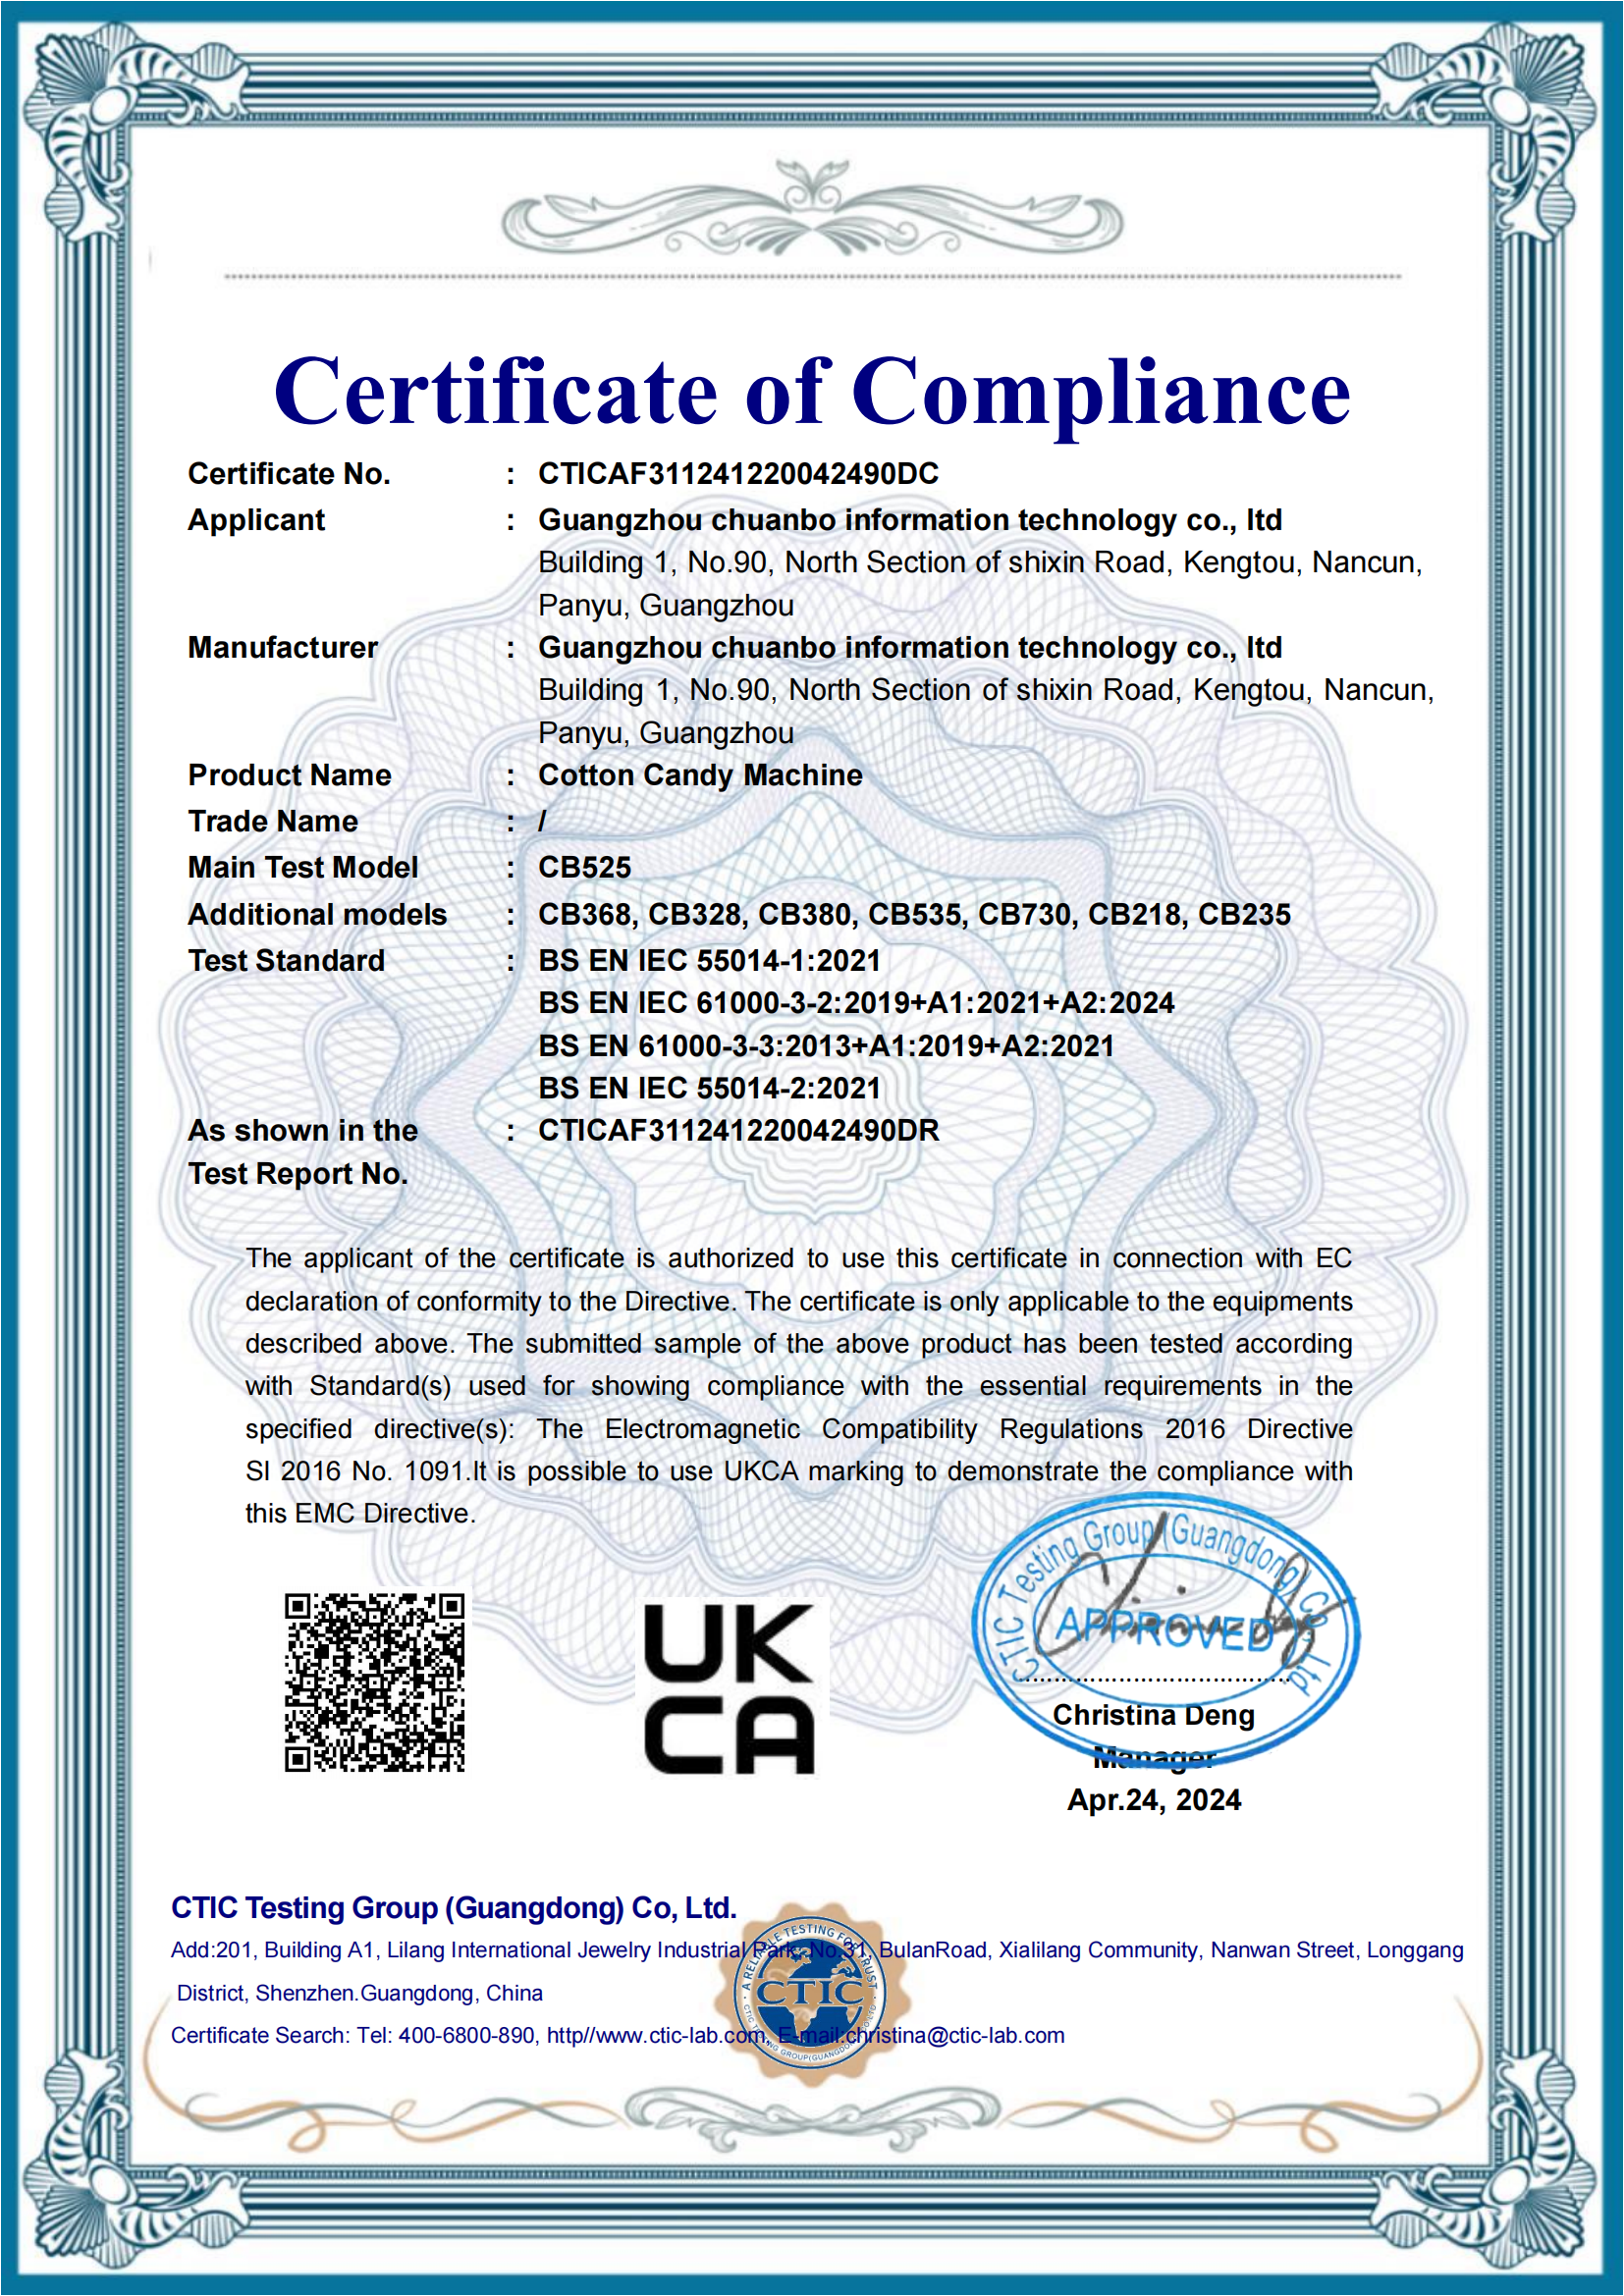
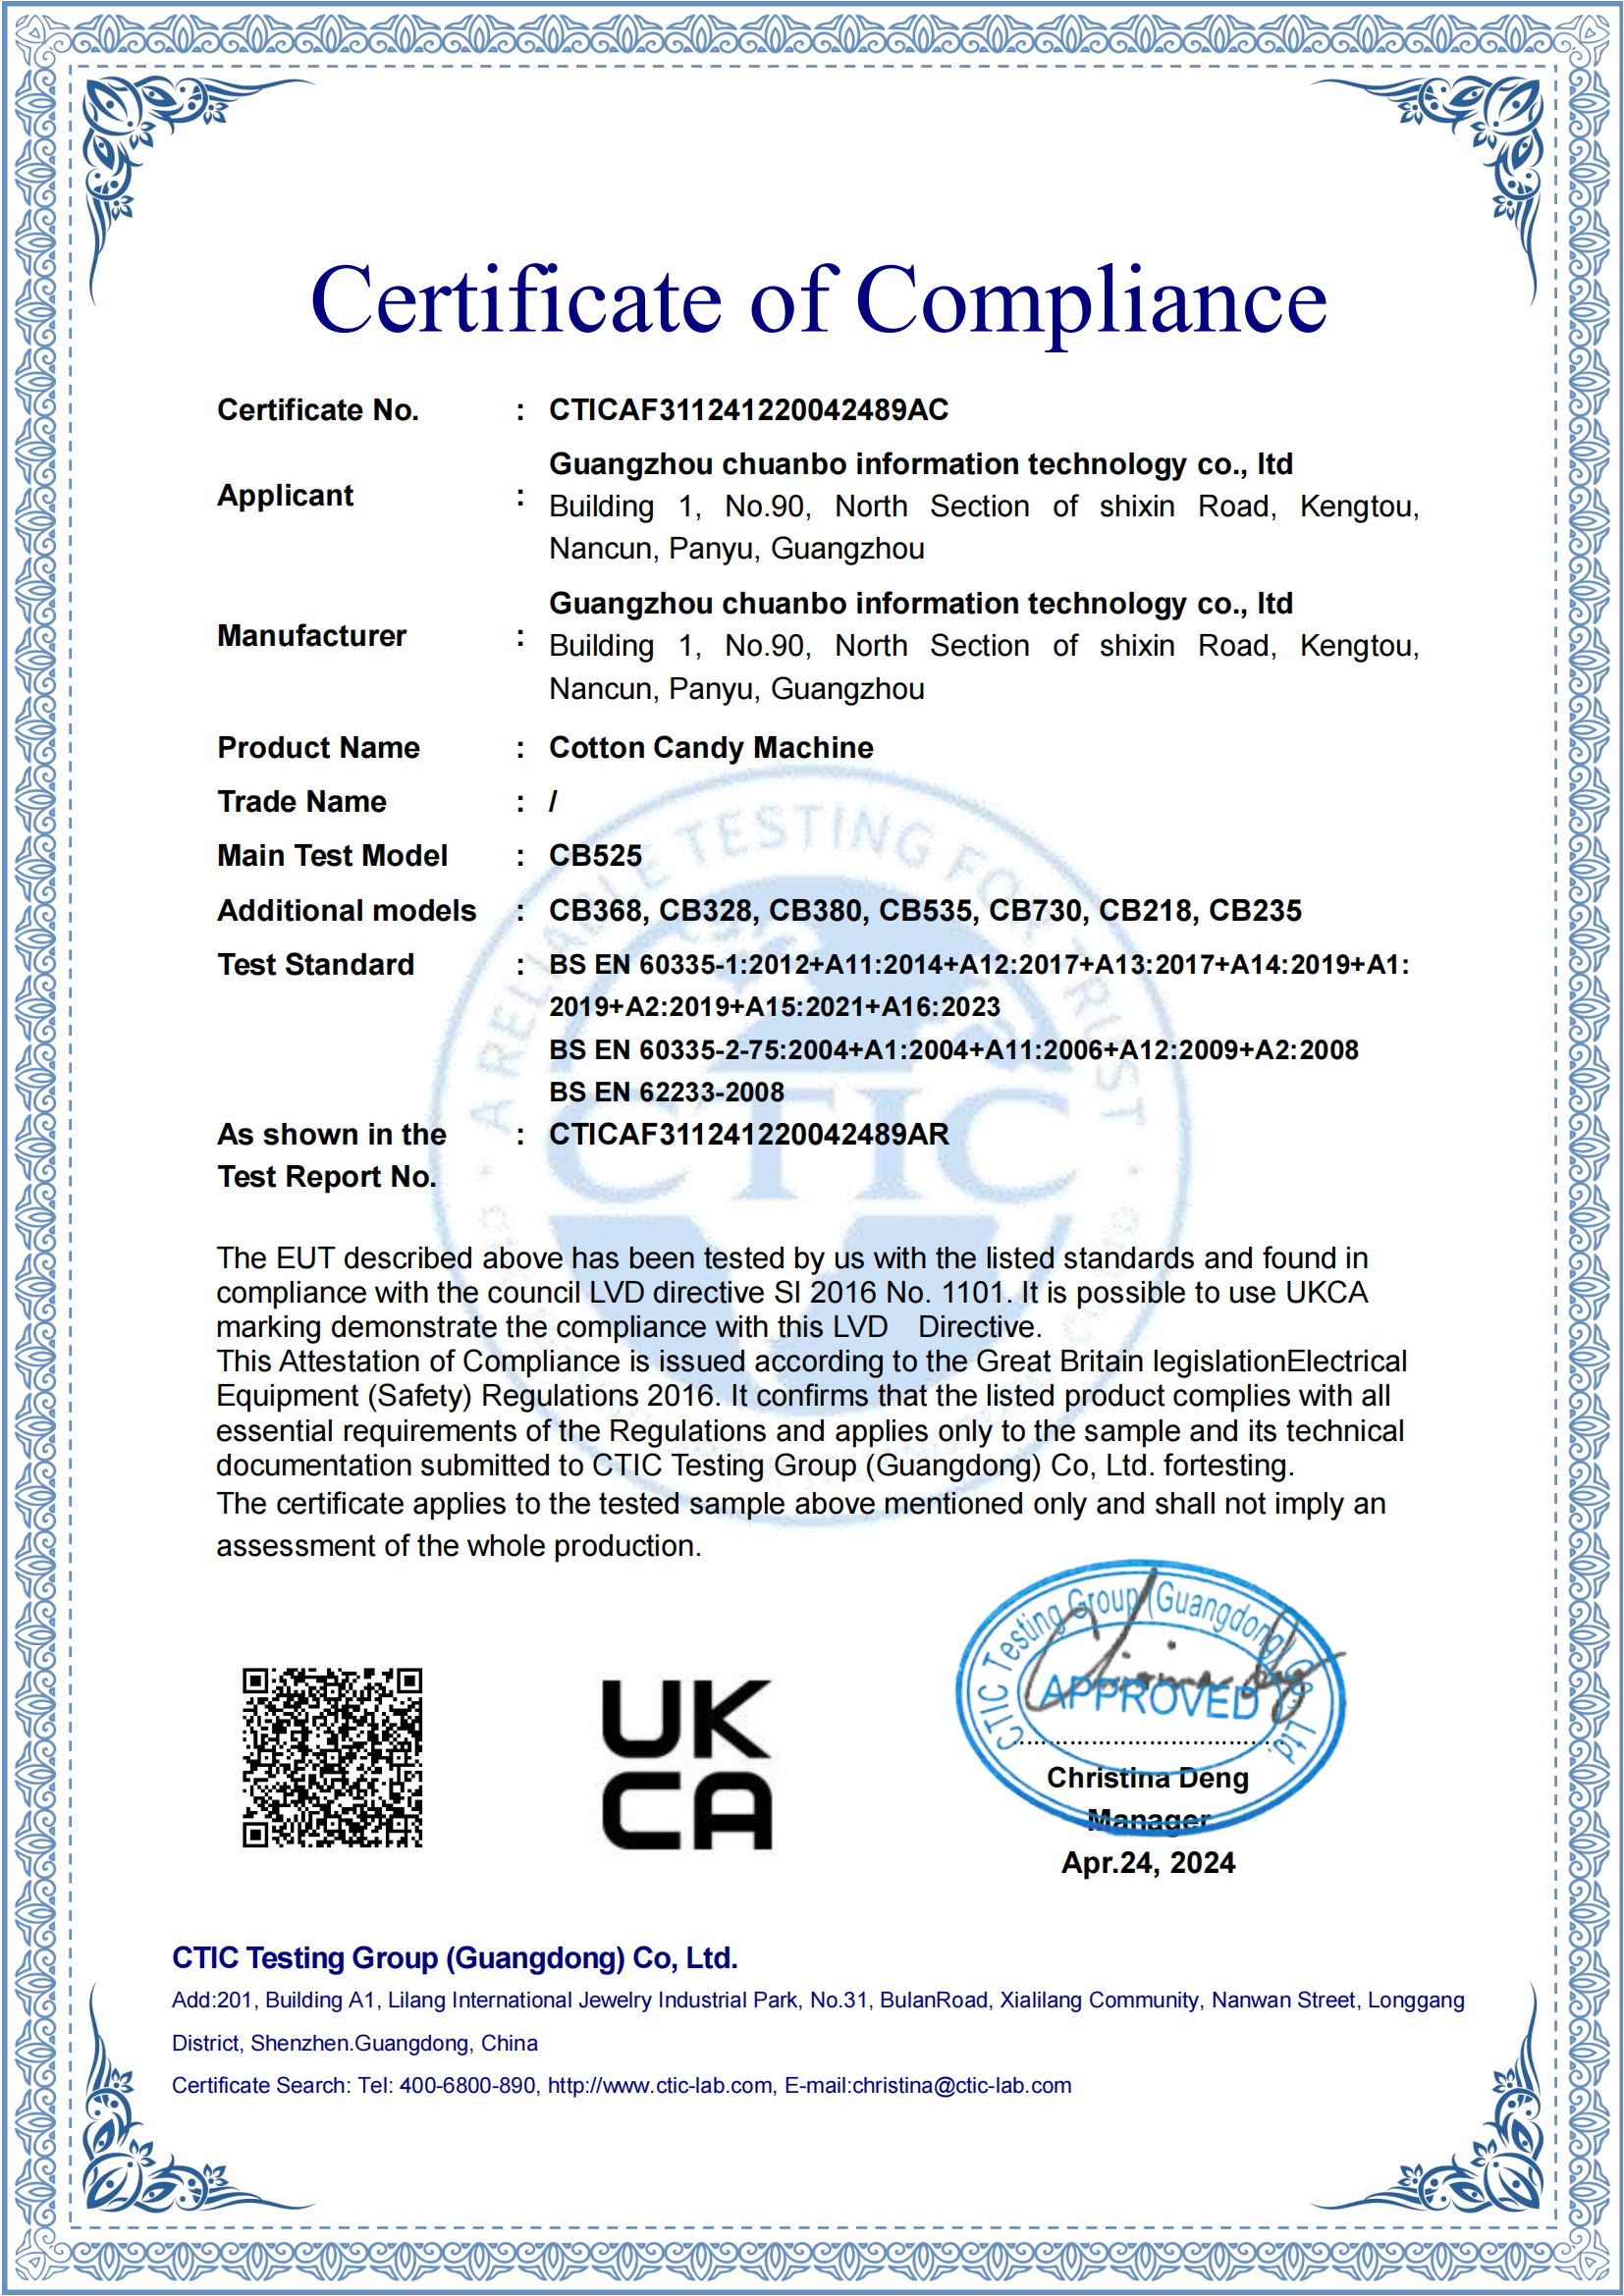
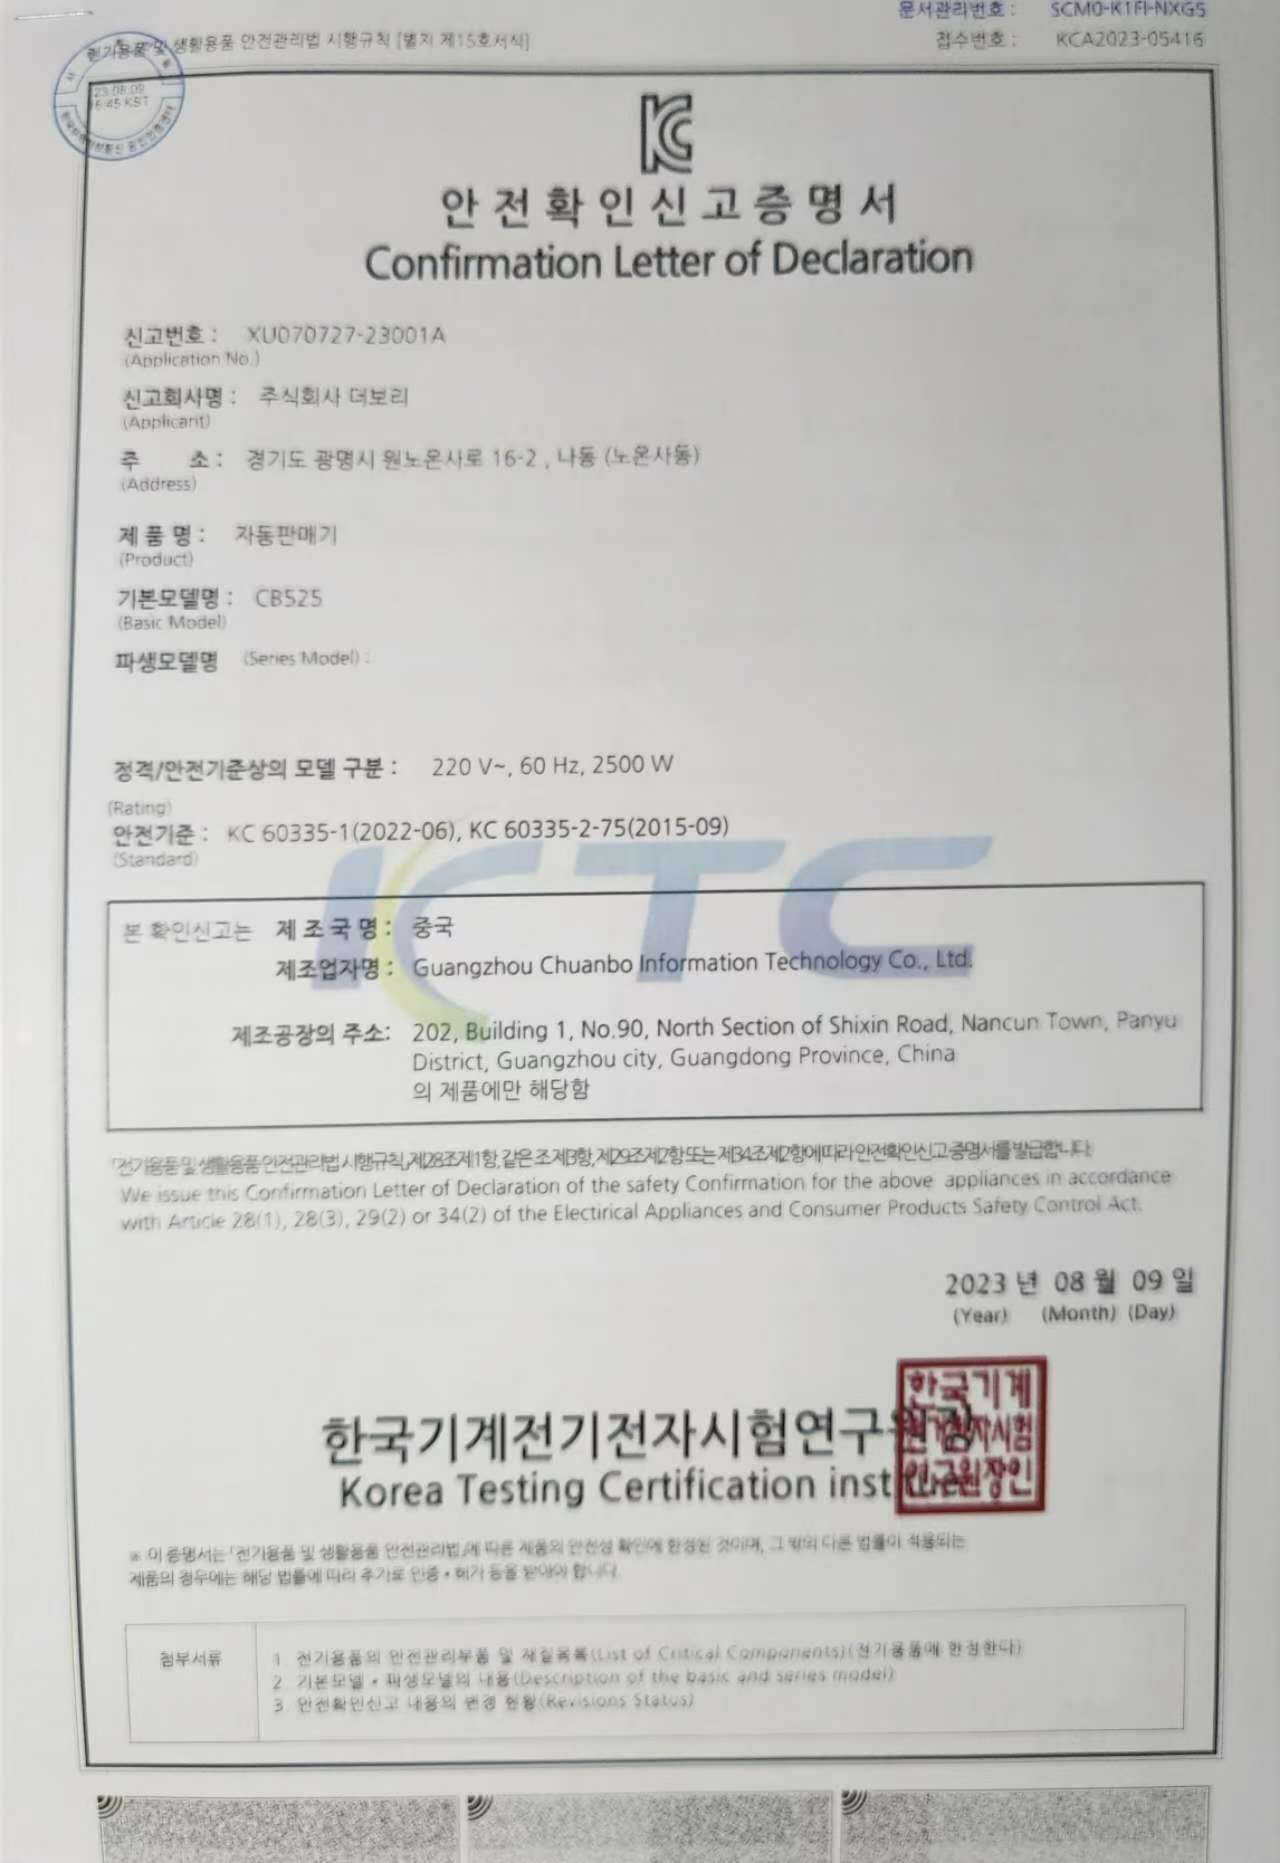
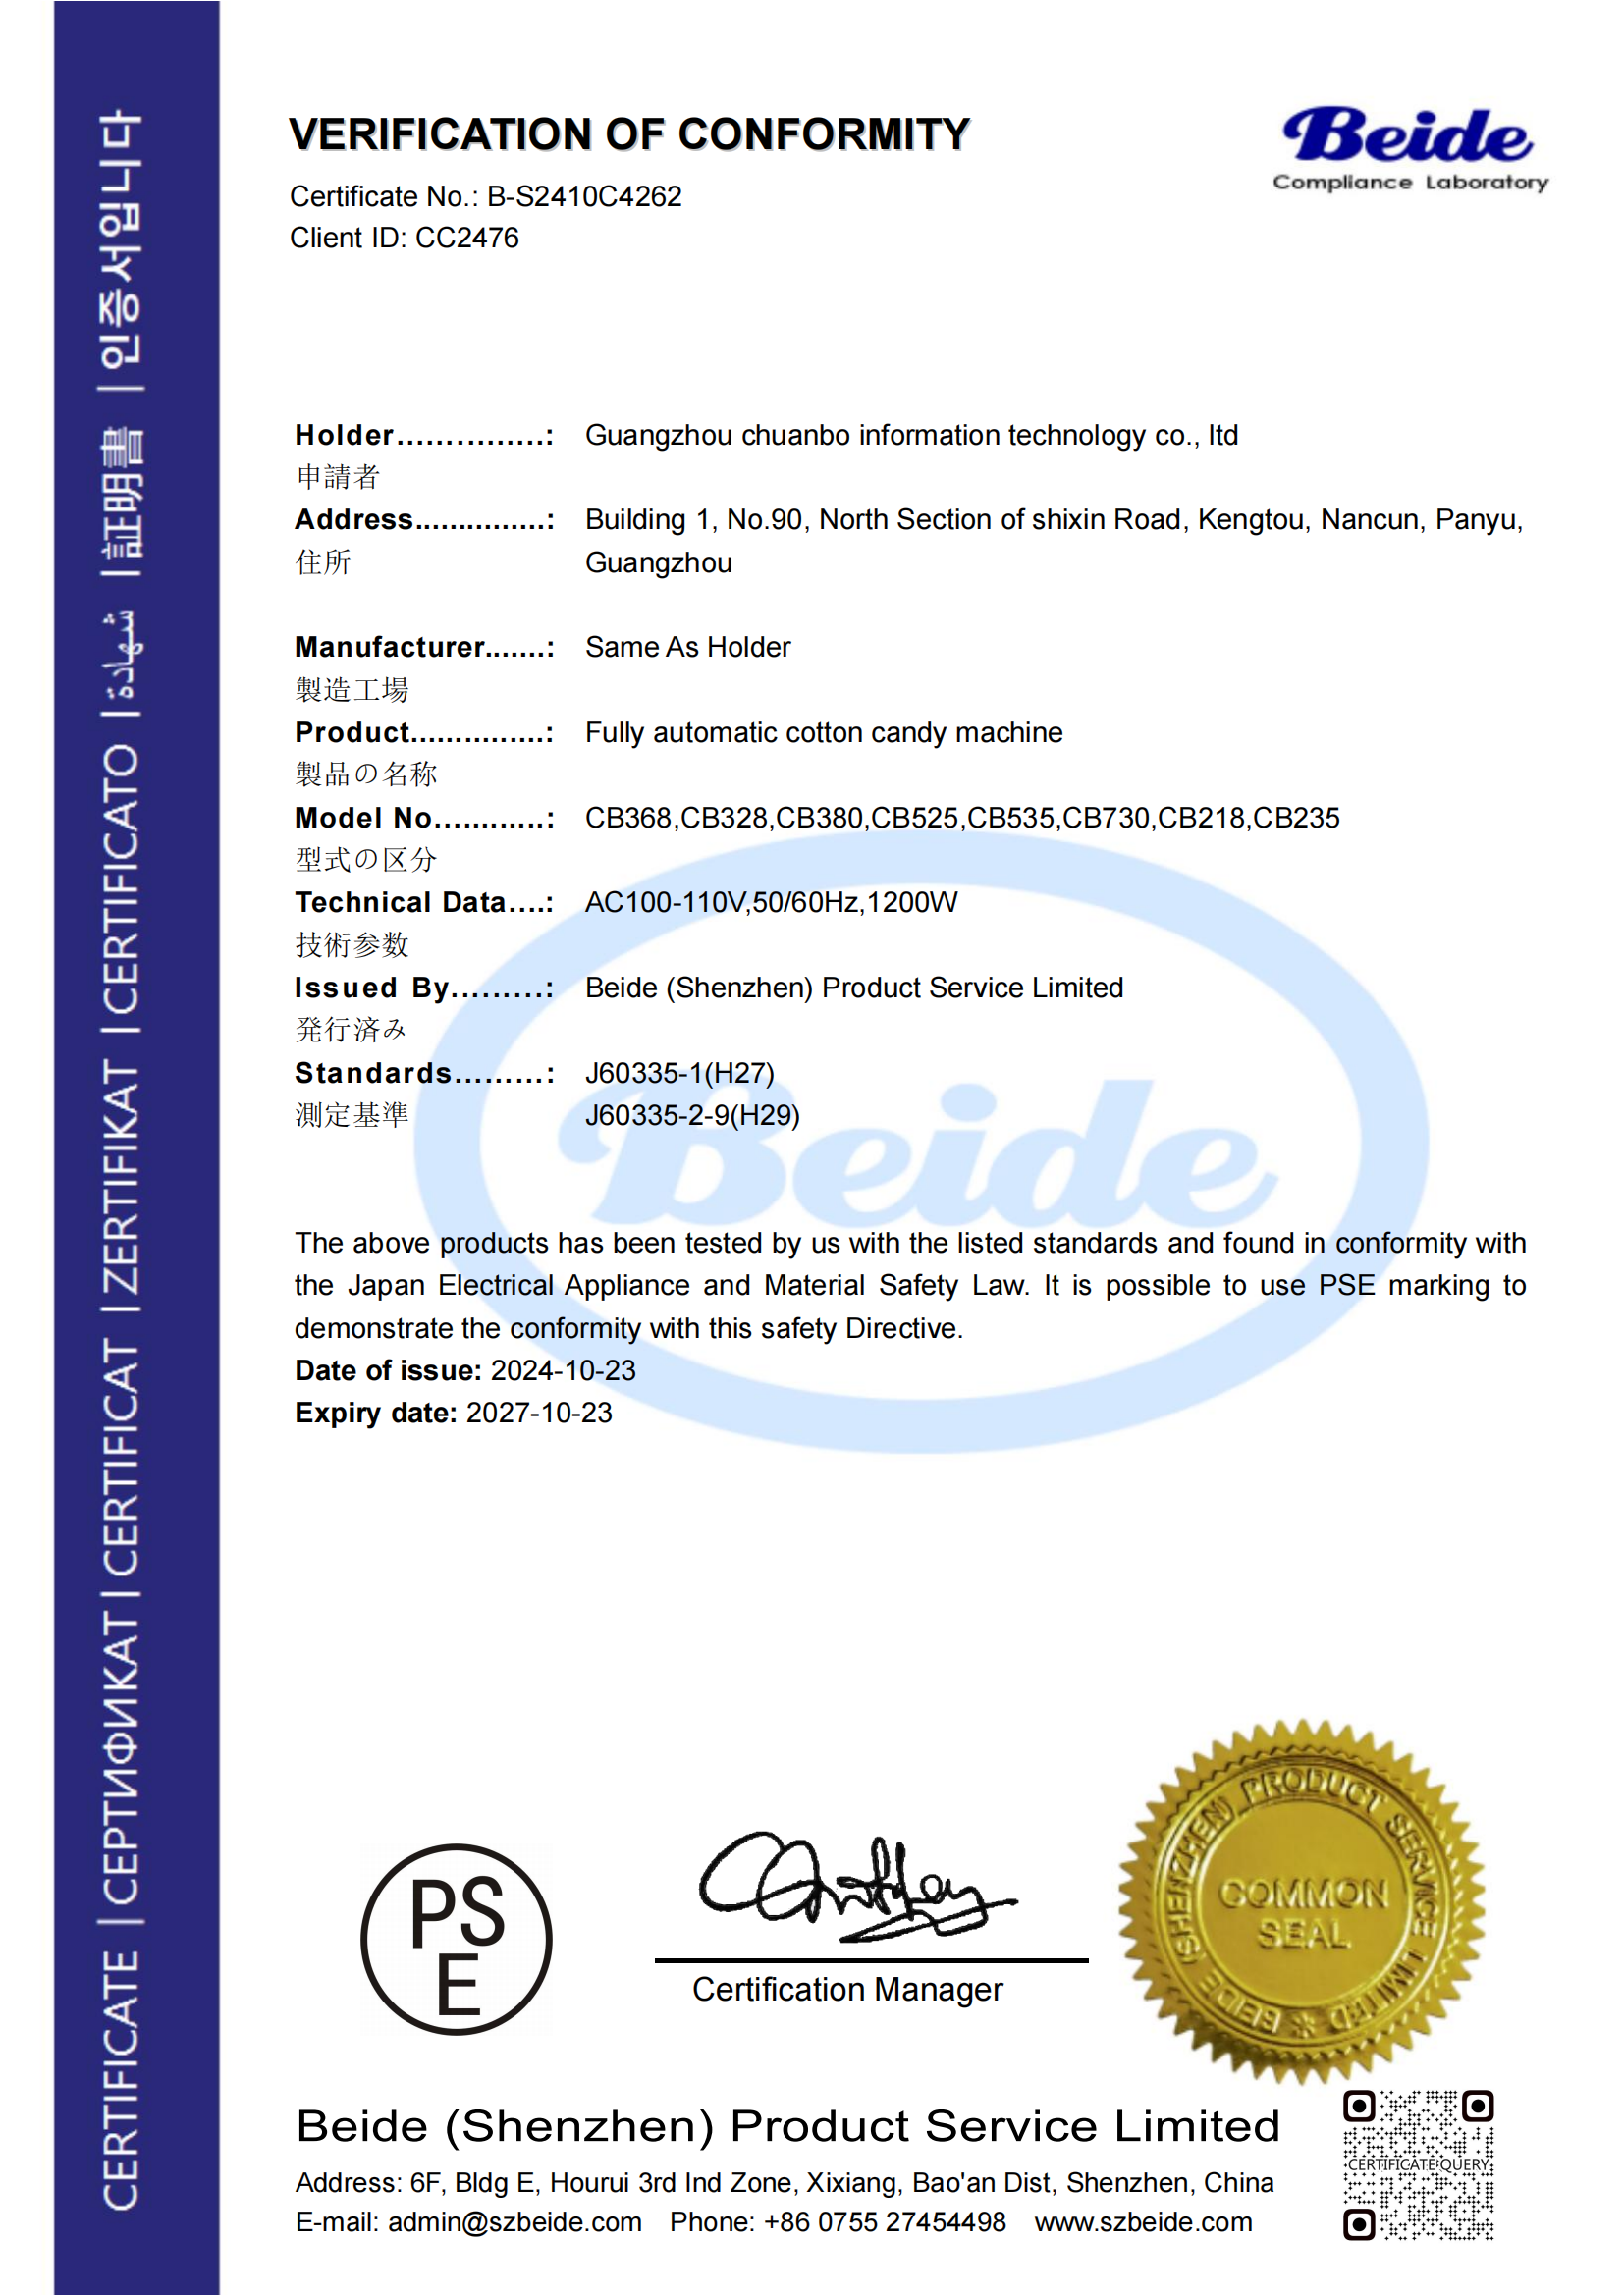
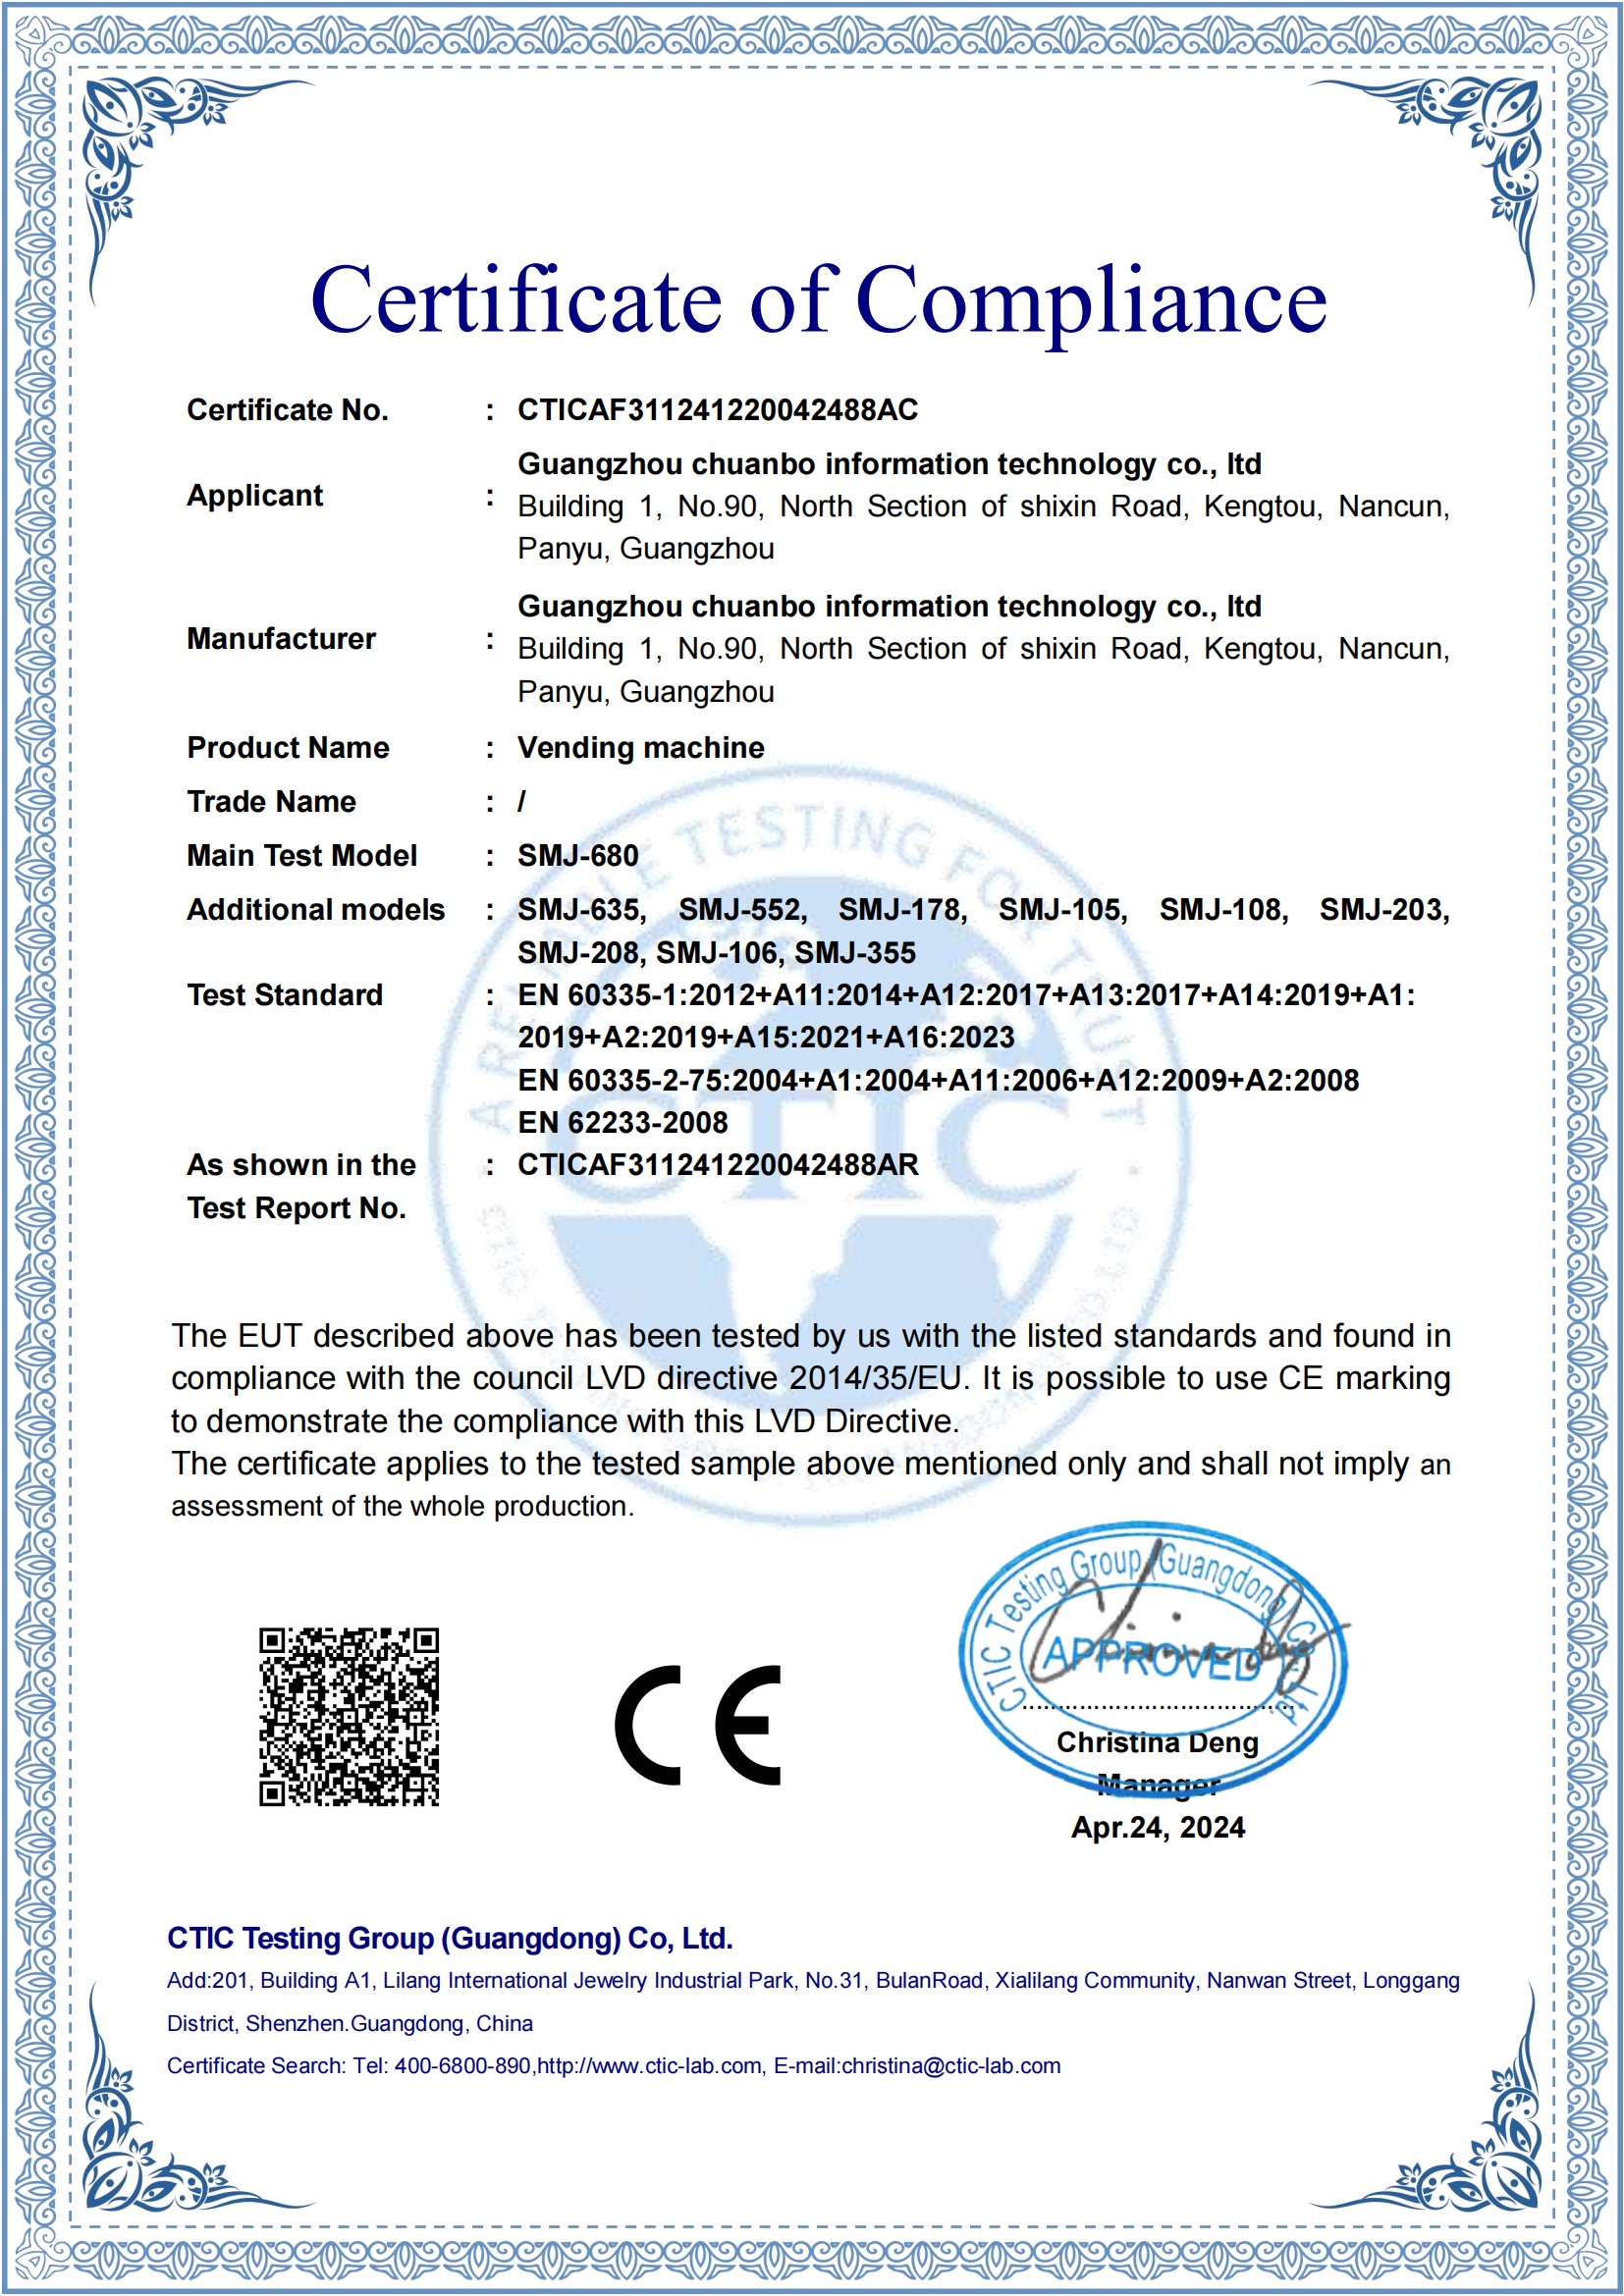
Quality assurance is embedded in every stage of our production workflow. From raw material traceability to full-unit inspection before dispatch, our dedicated QA/QC team guarantees compliance with global standards. Below are our verified international quality certifications:
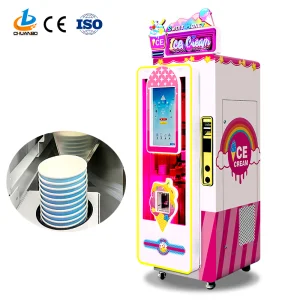
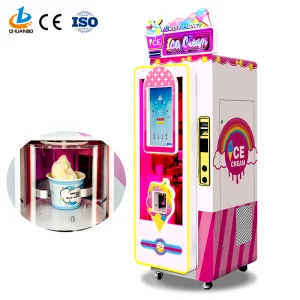
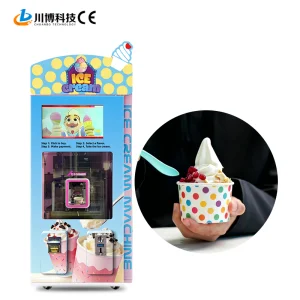
We provide light customization, sample processing, graphic processing, and complete on-demand engineering. Clients can customize exterior branding, touch screen user interfaces (SDK integration), payment gateway integrations (Nayax, MDB protocol), and flavor configurations to match specific market preferences.
Our cloud-based telemetry platform enables operators to monitor machine status, ingredient inventory levels, daily sales revenue, and error diagnostics remotely via PC or mobile devices. This minimizes downtime and optimizes restocking schedules.
Our commercial food machinery complies with strict global regulatory standards. We hold valid ISO 9001, CE, RoHS, RCM, CB, UL, UKCA, KC, and PSE certifications, ensuring hassle-free customs clearance and legal operation in North America, Europe, Australia, East Asia, and the Middle East.
Backed by 3,000 square meters of production space, robust supply chain partnerships with over 30 verified component suppliers, and 11 years of export experience, we ensure efficient production turnaround times and comprehensive after-sales technical support for global brand businesses, retailers, and wholesalers.